Séchoir à Rouleaux vs. Séchoir à Tapis: Guide Comparatif Industriel Complet
Étude comparative approfondie entre séchoirs à rouleaux et séchoirs à tapis métallique. Rendement thermique, séchage des faces décoratives et coûts d'exploitation.
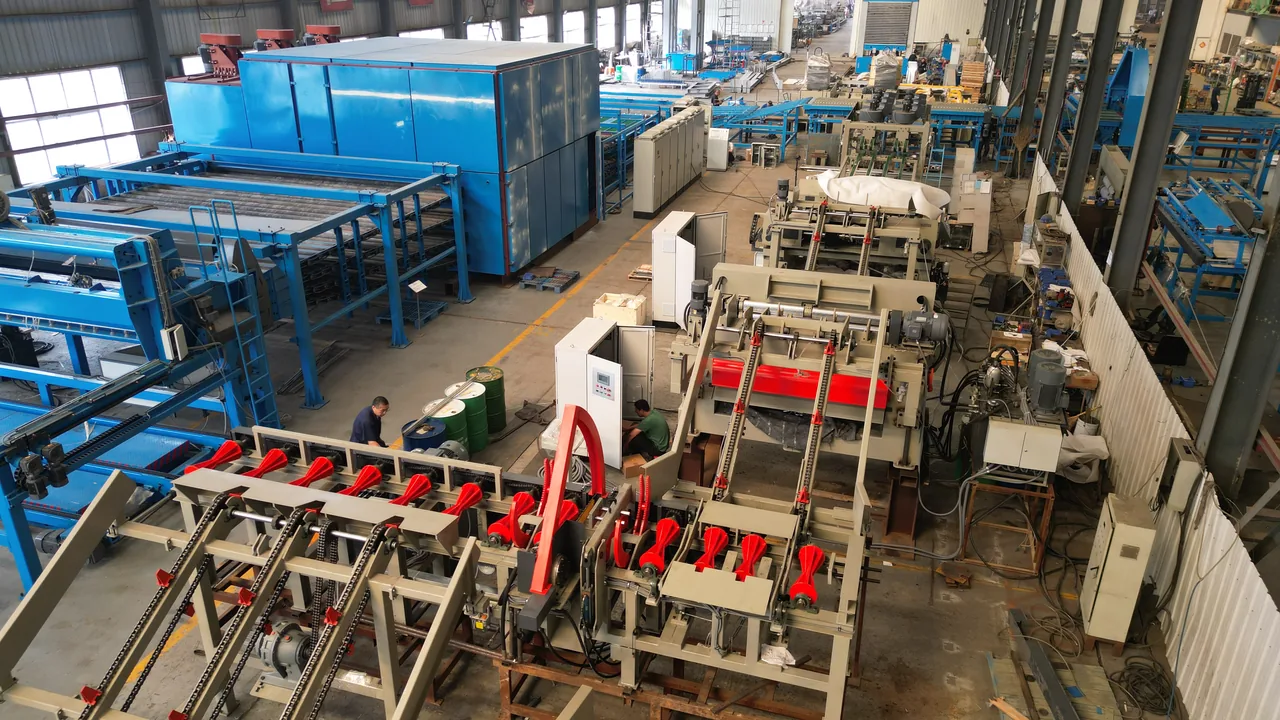
In rotary veneer and plywood production, veneer drying accounts for over 60% of total plant thermal energy consumption and represents the most critical bottleneck for surface quality. Excess moisture causes catastrophic delamination ("steam blisters") during subsequent hot pressing, while over-drying makes wood sheets brittle, leading to severe edge splits and glue starvation.
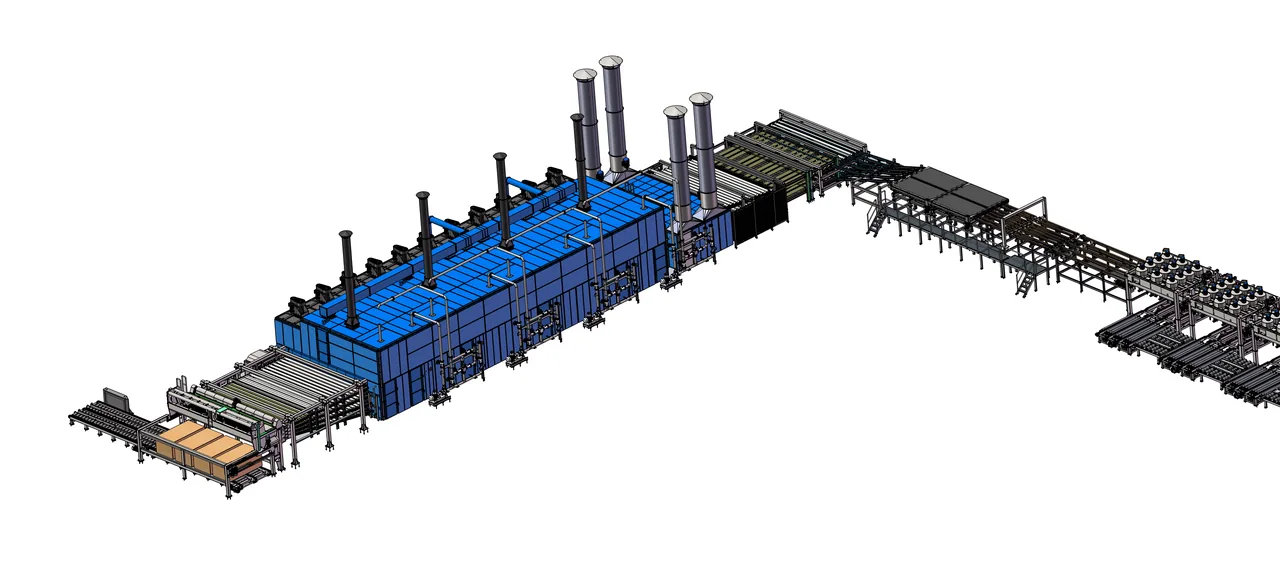
When configuring a fully automatic veneer drying line, mill managers and plant engineers invariably face a primary equipment selection decision: Should you invest in a roller-type veneer dryer, a mesh belt dryer, or a combination hybrid system?
This guide provides an exhaustive engineering analysis of mechanical mechanisms, drying kinetics, wood species suitability, and lifecycle operating costs to help you determine the optimal configuration for your mill.
1. Mechanical Mechanisms: How They Move and Dry Veneer
The fundamental operational distinction between roller and mesh belt dryers lies in how sheets are conveyed through the heated jet chambers:
Roller-Type Veneer Dryers
- ✓Conveying Mechanism:
Veneer sheets travel between pairs of horizontally stacked, motor-driven steel rollers. Upper rollers exert continuous, controlled gravitational and mechanical pressure directly onto the top face of the veneer.
- ✓Flattening Effect:
Because high moisture veneers naturally curl and shrink non-uniformly as water evaporates, the continuous contact with heated steel rollers provides an ironing effect. This forces the veneer flat throughout its thermal transit, dramatically minimizing wavy edges and post-drying warp.
- ✓Jet Air Delivery:
High-velocity hot air jets (heated by thermal oil, steam, or biomass flue gas) are discharged through precision aerodynamic nozzles directly above and below the veneer surface, stripping the boundary moisture layer at speeds up to 25–35 m/s.
Mesh Belt Veneer Dryers
- ✓Conveying Mechanism:
Veneer is supported and conveyed between two continuous woven wire mesh belts (usually high-tensile stainless or carbon steel).
- ✓Tension-Free Transport:
Unlike solid steel rollers, the flexible mesh belts cradle delicate veneer gently. There are no rigid pinch points, which makes mesh belt systems exceptionally gentle on thin, brittle, or irregularly clipped face veneers.
- ✓Surface Protection:
Mesh belt dryers eliminate the risk of roller surface contamination or mechanical imprint marks on sensitive decorative hardwood veneers (such as natural oak, walnut, or birch face veneers).
2. Engineering Comparison: Roller vs. Mesh Belt
| Feature / Metric | Roller Veneer Dryer | Mesh Belt Veneer Dryer | Hybrid Roller-Mesh System |
|---|---|---|---|
| Primary Veneer Type | Core veneer, cross-band, thick face | Thin decorative face, sensitive veneer | Mixed production (Face + Core) |
| Veneer Thickness Range | 1.0 mm – 5.0 mm | 0.25 mm – 1.8 mm | 0.3 mm – 4.5 mm |
| Flattening Capability | Superior (Ironing Effect) | Moderate (Gentle restraint) | Excellent |
| Jam Frequency on Random Widths | Low (with automatic infeed) | Extremely low | Low |
| Thermal Transfer Efficiency | High (Convection + Roller Conduction) | High (Pure Jet Convection) | High |
| Belt/Roller Wear & Replacement | Long life (Heavy-duty steel pipe) | Mesh replacement every 2–4 years | Moderate |
| Energy Consumption per m³ | Standard | ~5–8% higher fan draw | Balanced |
| Capital Investment (CAPEX) | Standard industrial baseline | ~12–18% higher | Premium turnkey |
3. Veneer Species and Thickness Suitability
When to Choose a Roller Dryer
- 1High-Volume Core Veneer Production:
If your mill primarily peels eucalyptus, acacia, rubberwood, pine, or poplar with thicknesses between 1.2 mm and 3.6 mm, a 3-deck or 4-deck roller dryer is the undisputed industry standard. The heavy rollers ensure flat, stackable sheets that feed smoothly into automatic glue spreaders.
- 1Fast-Growing Plantation Hardwoods:
Species with high internal tension tend to warp aggressively during rapid moisture evaporation. The mechanical restraint of heavy rollers counteracts this distortion.
- 1Heavy Structural Plywood & LVL:
Thick veneers (up to 4.5 mm) used in structural plywood or Laminated Veneer Lumber (LVL) require substantial contact pressure to maintain uniform thickness.
When to Choose a Mesh Belt Dryer
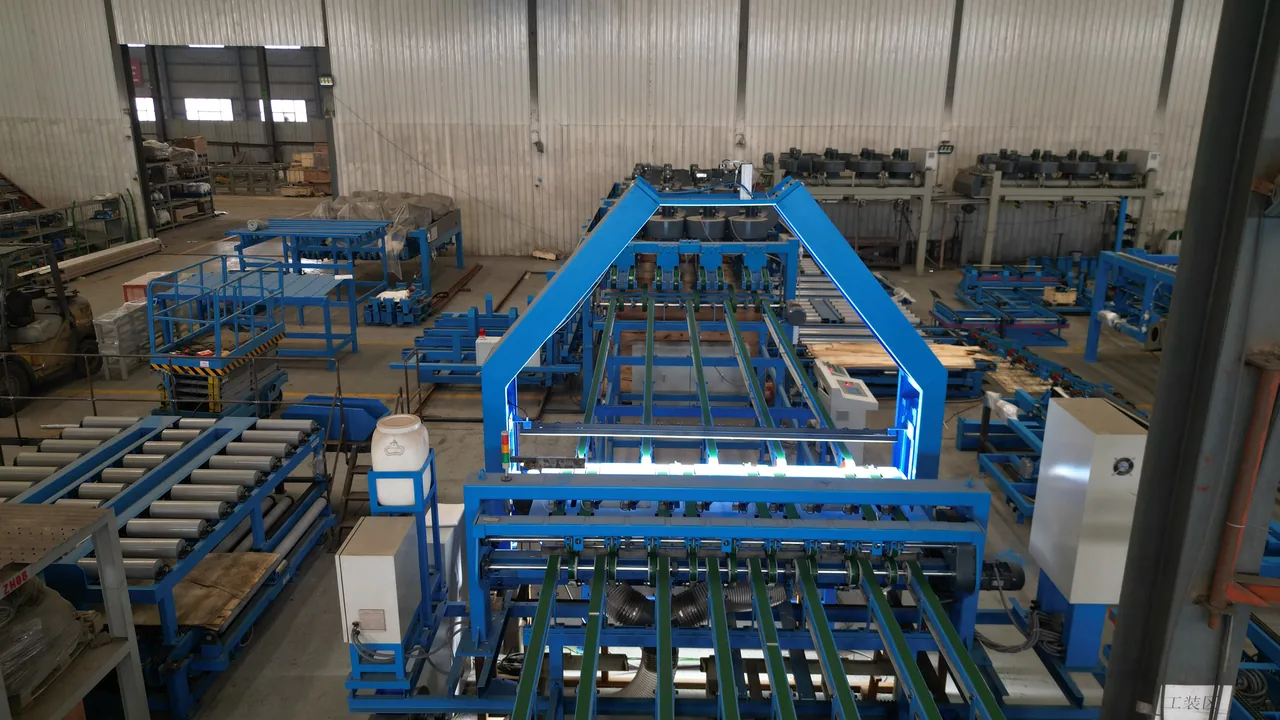
- 1Ultra-Thin Decorative Face Veneers:
When drying face veneers thinner than 0.6 mm, roller dryers can occasionally catch sheet leading edges or cause roller wrap-arounds. Mesh belts provide continuous 100% surface support, completely preventing jam-ups.
- 1Irregularly Shaped or Tender Veneers:
Pre-clipped veneers with wavy natural grains or random small pieces stay securely sandwiched between the upper and lower mesh screens without shifting or overlapping.
4. Energy Efficiency and Heat Source Integration
Modern veneer drying requires vast energy reserves. Hanvy continuous dryers are engineered to integrate seamlessly with various heating systems:
- ✓Biomass Burner Direct Flue Gas Heating:
Utilizes factory wood residue (bark from your hydraulic log debarker, dry veneer cut-offs, and lathe cores) to generate clean, high-temperature furnace gases, cutting fossil fuel costs to near zero.
- ✓Thermal Oil Radiator Heat Exchangers:
Provides precise temperature zoning across multiple drying decks (e.g., Zone 1 at 180°C for rapid initial evaporation; Zone 4 at 130°C for gentle equalization).
- ✓Steam Coils:
Ideal for mills operating high-pressure steam boilers.
For a detailed evaluation of thermal oil vs steam heat transfer in panel pressing and drying, see our companion analysis on Thermal Oil vs. Steam Plywood Heating Systems.
5. Frequently Asked Questions (FAQ)
Can a roller dryer dry thin face veneer without cracking?
Yes, with precision roller gap adjustment and speed synchronization. However, for continuous production of face veneer under 0.5 mm, an upper-mesh / lower-roller hybrid dryer or dedicated mesh belt dryer offers superior yield and lower scrap rates.
What is the ideal veneer moisture content after drying?
For urea-formaldehyde (UF) and melamine-urea-formaldehyde (MUF) resin bonding, target moisture content is 8% to 12%. For exterior phenol-formaldehyde (PF) resins, 6% to 8% is recommended to prevent steam blowout during hot press cycles.
How does automatic infeed improve drying efficiency?
An automatic veneer dryer feeder tightly regulates sheet spacing on each deck, increasing chamber fill rates from 65% (manual feeding) to over 92%, resulting in a 25–35% increase in daily output with zero extra fuel consumption.
Maximize Your Mill's Drying Performance
Hanvy Machinery designs and manufactures custom 2-deck, 3-deck, 4-deck, and 5-deck continuous roller and mesh belt veneer drying lines tailored to your target wood species, daily peeling capacity, and factory footprint.
Équipe d'Ingénierie Hanvy Machinery
Conçu avec plus de 30 ans d'expertise dans la fabrication de machines pour contreplaqué. Plus de 500 lignes installées dans 69 pays.
Guides Techniques Recommandés

Ligne de Déroulage sans Broche: Guide de Configuration 4 ft vs. 8 ft, Rendement et Économie
Rentabilité industrielle des formats 4 et 8 pieds: calcul des économies de bois d'œuvre, intégration d'empileurs à dépression et cadences d'usine.

Séchoir à Rouleaux vs. Séchoir à Tapis: Consommation d'Énergie, Rendement et Guide de Choix
Spécifications des séchoirs Hanvy séries HG: tubes sans soudure 100 mm, roulements graphite et téflon, et réduction des consommations thermiques.
Presse Hydraulique Automatique pour Contreplaqué: Optimisation des Cycles et Courbes de Pression
Maîtrise du pressage à chaud industriel: transmission thermique au cœur du panneau, polymérisation des colles et cadences de chargement automatique.