Veneer Scarf Jointing vs. Core Composing: How to Produce Oversized & High-Strength Plywood Panels
Veneer scarf jointing vs. core composing guide: learn how 1:10 slope bevel milling delivers 95% solid wood strength for oversized container flooring and marine plywood panels.

In commercial plywood and laminated veneer lumber (LVL) manufacturing, standard rotary peeling lathes typically output wood sheets limited to 4ft (1,300 mm) or 8ft (2,600 mm) in length. However, international infrastructure, heavy-duty container flooring, modular housing, and commercial boat-building require continuous, oversized panels reaching lengths of 9ft, 10ft, 12ft (3,660 mm), or even 18 meters.
To manufacture these long-length panels without compromising mechanical tensile strength, mills utilize veneer scarf jointing and automatic core composing. Understanding the engineering differences between these two jointing technologies is essential for selecting the correct machinery.
Technical Comparison: Scarf Jointing vs. Finger Jointing vs. Edge Composing
| Feature / Metric | Veneer Scarf Jointing (Bevel Milling) | Automatic Core Composing (Edge Splicing) | Finger Jointing (Structural Timber) |
|---|---|---|---|
| Joint Geometry | 1:8 to 1:12 slope precision feather-edge bevel | Square butt joint (90° edge-to-edge) | Interlocking multi-tooth fingers (10–25 mm depth) |
| Grain Orientation | End-to-end longitudinal grain extension | Side-by-side lateral width extension | End-to-end solid lumber / thick veneer (> 4 mm) |
| Typical Veneer Thickness | 1.0 mm to 3.6 mm rotary veneer | 1.2 mm to 3.2 mm green or dry veneer | 4.0 mm to 30 mm lumber flitches |
| Adhesive Application | Waterproof Phenolic (PF) or Melamine resin | Hot-melt thermal thread / Spot PVA adhesive | Resorcinol-formaldehyde / Structural PUR |
| Joint Tensile Strength Ratio | 85% – 95% of solid wood strength | Non-structural (relies on hot-press consolidation) | 75% – 88% of solid wood strength |
| Primary End Products | Marine plywood, container flooring, LVL beams | Standard 4x8 ft core boards for commercial panels | Finger-jointed door cores, structural joists |
| Primary Machinery Line | Veneer Scarfing Saw + Hot Scarf Press | Core Veneer Composer Line | Finger Joint Shaper & Hydraulic Assembler |
4 Engineering Steps of the Industrial Veneer Scarf Jointing Process
The scarf jointing line operates as a synchronized four-stage automated workflow:
| Stage | Operation & Machinery | Engineering Mechanism & Quality Benchmark |
|---|---|---|
| Step 1: Alignment & Clamping | Laser Projection Alignment & Hydraulic Clamp | High-precision laser guides square veneer ends; top clamp holds sheets firmly to eliminate diagonal skew. |
| Step 2: Precision Bevel Milling | Dual High-Speed Diamond Scarfing Saws | Twin cutter heads plane an exact 1:10 slope bevel (25 mm taper on 2.5 mm veneer) without tearing feather tips. |
| Step 3: Automated Adhesive Coating | Precision Micro-Metering Glue Applicator | Even spread of waterproof phenolic (PF) or melamine resin applied exclusively along the milled taper interface. |
| Step 4: Hot Splicing & Curing | Narrow Single-Daylight Hydraulic Scarf Press | Applies 140°C platen temperature and 1.5 MPa specific pressure for 8–15 seconds, curing joint to 95% solid wood strength. |
1. The Scarf Angle Ratio Principle (Why 1:8 to 1:12 Slope is Critical)
A butt joint (90° cut) has virtually zero tensile strength because end-grain wood pores cannot establish structural adhesive shear bonds. By milling the veneer edge into a long, tapered wedge with a slope between 1:8 and 1:12 (e.g., for a 2.5 mm veneer, the tapered bevel length is 25 to 30 mm), the glued interface acts under shear stress rather than tension. This delivers joint strength approaching 95% of solid, uncut wood grain.
2. High-Speed Scarf Milling & Feather-Edge Protection
A dedicated Veneer Scarf Milling Machine utilizes twin high-speed diamond-tipped cutter heads. The primary hogger removes bulk wood, while the precision finishing head planes a glass-smooth surface without tearing delicate feather tips.
3. Rapid Hydraulic Hot Scarf Pressing
Once resin is applied, the beveled overlap is clamped inside a continuous or cycling Hydraulic Scarf Press. Controlled hydraulic pressure ensures zero glue-line thickness variation, preventing thick spots that could cause panel indentations during final multi-layer hot pressing.
Automatic Core Veneer Composing: Eliminating Core Voids
While scarf jointing extends veneer lengthwise, an Automatic Core Veneer Composer solves the opposite problem: assembling random, narrow rotary-peeled strips into solid, continuous 4x8 ft inner core sheets.
Why Modern Plywood Mills Replace Manual Taping with Composers:
- 1Zero Overlaps & Core Voids: Optical sensors detect veneer thickness and edge alignment. Servo-driven feeding belts push edges tightly together before stitching, preventing hidden internal core voids that cause structural failure in concrete formwork.
- 2Thermal Thread vs. Spot Gluing: High-speed heating shoes melt fiberglass or polyester thermal thread into an alternating zig-zag pattern across the joint. The thread has no water content, preventing steam blisters inside the hot press.
- 3Labor Savings: A single automated composer replaces 4 to 6 manual assembly workers while increasing sheet jointing output to 2 to 3 full 4x8 ft sheets per minute.
Frequently Asked Questions (FAQ)
Why is scarf jointing required for container flooring and marine plywood?
International standards for cargo container flooring (such as IICL specifications) and marine plywood (BS 1088) require high bending stiffness (MOE) and modulus of rupture (MOR). Butt joints or random core gaps cause localized flex cracking under heavy forklift axle loads. Scarf jointed continuous veneer plies ensure continuous grain load distribution throughout the panel length.
Can wet (green) veneer be scarf jointed?
No. Veneer must be dried to 8%–10% moisture content prior to scarfing. High moisture causes adhesive dilution, poor chemical polymerization, and severe steam blowout when clamped under the high-temperature scarfing press.
What is the maximum panel length achievable with a veneer scarf jointing line?
Technically, scarf jointing can produce endless, continuous veneer strips. In practice, panel length is determined by the downstream press capacity or cutoff saw settings, commonly producing 3,050 mm (10ft), 3,660 mm (12ft), or continuous rolls for laminated veneer lumber (LVL) beams.
❓ Foire Aux Questions
Q:Why is scarf jointing required for container flooring and marine plywood?
International standards require continuous grain load distribution. Scarf joints provide 85-95% of solid wood tensile strength, preventing flex cracking under forklift loads.
Q:Can wet (green) veneer be scarf jointed?
No. Veneer must be dried to 8%-10% moisture content prior to scarfing to prevent glue dilution and steam blowout in the press.
Q:What is the maximum panel length achievable with a veneer scarf jointing line?
Scarf jointing can produce endless veneer ribbons, commonly cut into 10ft (3,050 mm), 12ft (3,660 mm), or continuous rolls for laminated veneer lumber (LVL) beams.
Équipe d'Ingénierie Hanvy Machinery
Conçu avec plus de 30 ans d'expertise dans la fabrication de machines pour contreplaqué. Plus de 500 lignes installées dans 69 pays.
Guides Techniques Recommandés
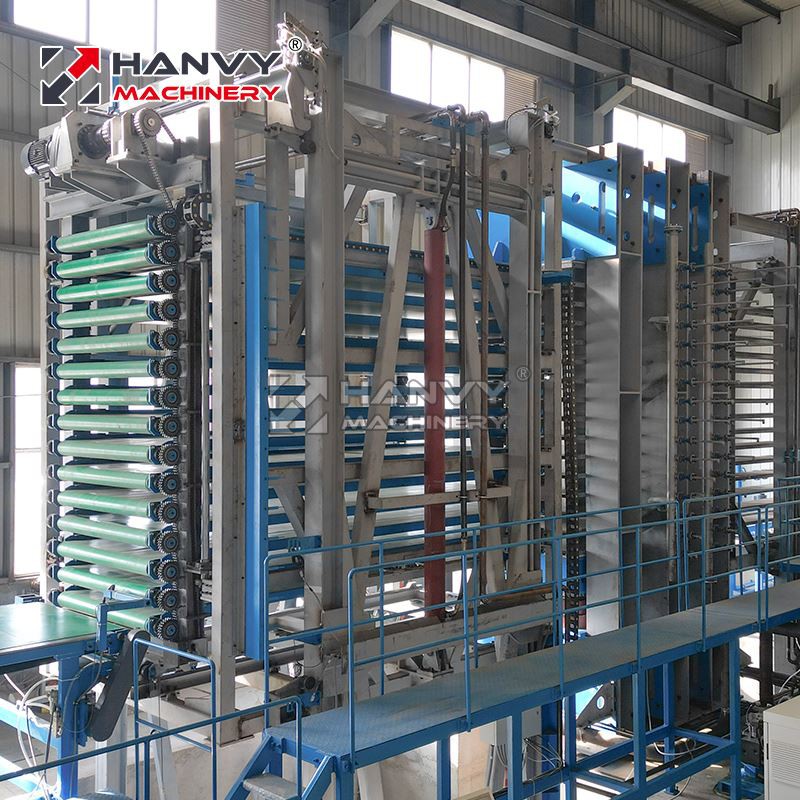
Short Cycle Melamine Laminating Hot Press Machine: The Complete Industrial Guide for Plywood & Panel Mills
Industrial guide to short cycle melamine laminating presses: technical specifications, fast pre-fill hydraulics, 15-30s press cycles, thermal oil platens, and economic ROI for plywood and panel mills.
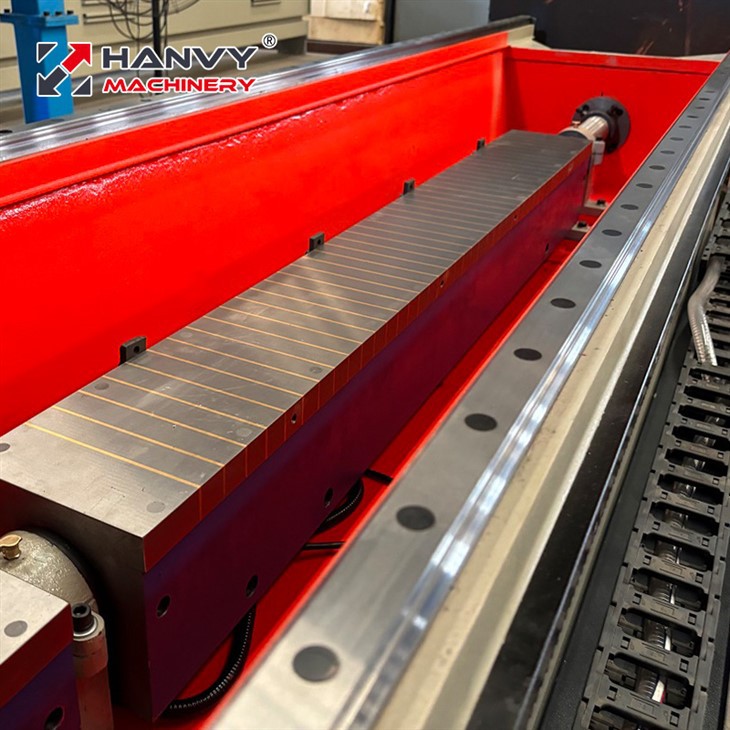
Troubleshooting Veneer Knife Grinding Defects: Edge Burning, Chatter Marks & Bowing Prevention
Engineering diagnostic guide for troubleshooting the 5 most critical veneer knife grinding failures: edge burning, chatter ripples, blade bowing, feathered burrs, and angle inconsistency.
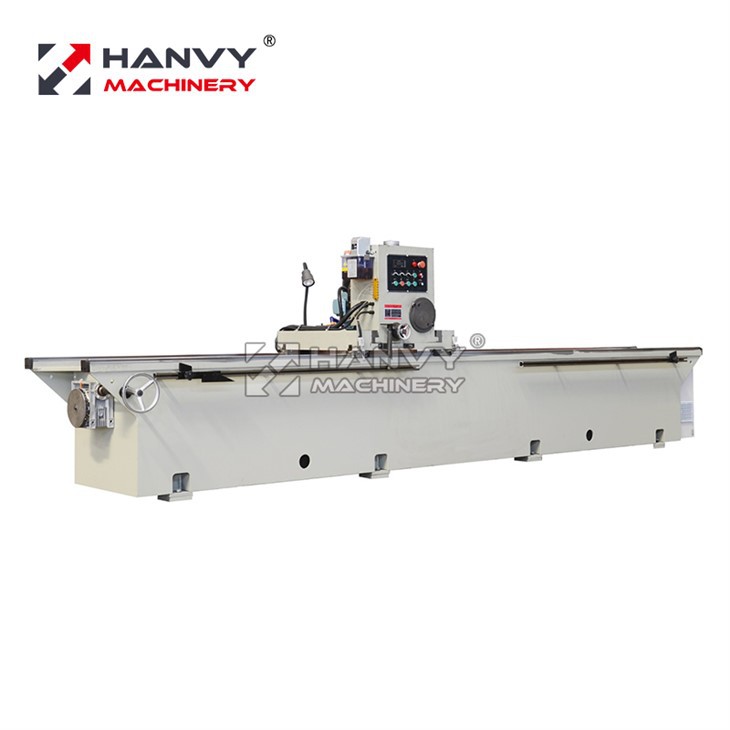
CNC Veneer Knife Grinder Selection & Maintenance: The Industrial Guide to Razor-Sharp Peeling Precision
Engineering selection guide for industrial veneer peeling knife grinders: electromagnetic chuck vs. mechanical beds, variable-speed traverse drives, CNC auto infeed cycles, and preventive maintenance SOP to achieve sub-micron blade straightness.