CNC Veneer Knife Grinder Selection & Maintenance: The Industrial Guide to Razor-Sharp Peeling Precision
CNC veneer knife grinder selection and maintenance guide: compare electromagnetic chuck sizes, automatic downfeed cycles, coolant systems, and daily millwright inspection SOP.
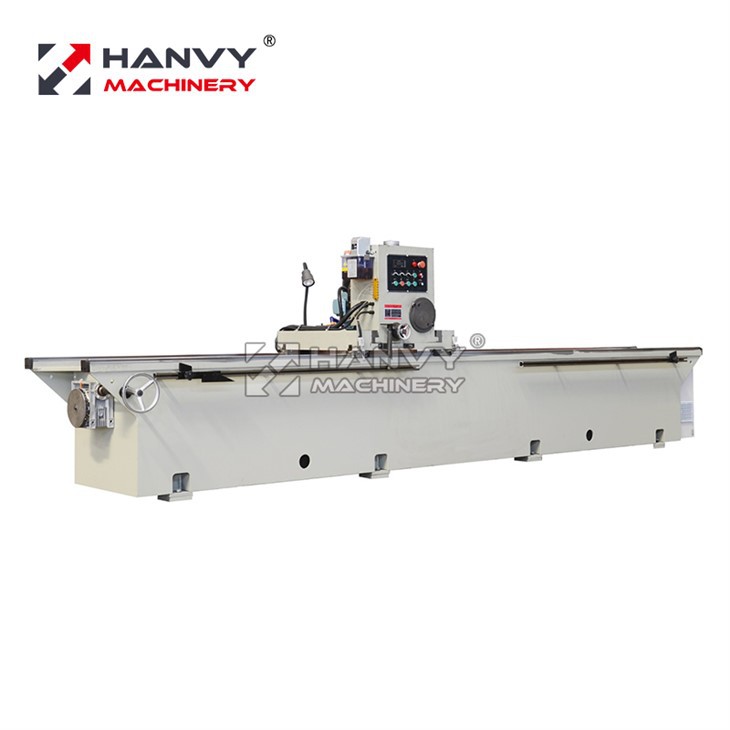
A veneer knife grinder (often referred to as an industrial guillotine blade sharpener or peeling lathe knife grinding machine) is the critical auxiliary equipment in a veneer and plywood mill that restores and maintains the primary cutting edge and bevel geometry of heavy alloy knives used on spindleless veneer peeling lathes and log clippers.
In commercial veneer production, knife sharpness directly governs green veneer thickness uniformity (achieving tight ±0.05 mm tolerances), surface smoothness, and motor power draw. Operating an un-calibrated or dull knife increases lathe drive motor load by up to 35%, accelerates pressure nose-bar wear, and causes deep micro-cracks on the veneer loose side.
Technical Specifications: Standard CNC Knife Grinder Models
Industrial knife grinding requires heavy cast-iron or stress-relieved steel beds with high vibration damping to eliminate chatter marks during high-speed wheel passes.
| Technical Parameter | Model HMD1500 (4ft Lathes) | Model HMD3000C (8ft Lathes) | Model HMD3600 (Heavy-Duty / Oversize) |
|---|---|---|---|
| Max. Grinding Length | 1,500 mm (59") | 3,100 mm (122") | 3,600 mm (142") |
| Grinding Width Capacity | Up to 250 mm | Up to 300 mm | Up to 320 mm |
| Electromagnetic Chuck Bed | Inclinable ±90°, 0°–30° bevel | Inclinable ±90°, 0°–30° bevel | Heavy magnetic chuck with digital readout |
| Grinding Wheel Diameter | Φ200 mm segmented cup | Φ250 mm segmented cup | Φ300 mm segmented ceramic cup |
| Wheel Spindle Motor Power | 5.5 kW / 7.5 HP | 7.5 kW / 10.0 HP | 11.0 kW / 15.0 HP |
| Carriage Traverse Speed | 3–18 m/min (Inverter VFD) | 3–20 m/min (Inverter VFD) | 2–22 m/min (Servo rack-and-pinion) |
| Auto Infeed Downfeed Rate | 0.005–0.05 mm per stroke | 0.002–0.03 mm per stroke | 0.001–0.02 mm precision finishing |
| Coolant Reservoir Capacity | 120 Liters with paper filter | 200 Liters dual-stage magnetic | 300 Liters centrifugal separation |
| Machine Total Weight | 3,800 kg | 6,500 kg | 8,200 kg |
4 Key Engineering Selection Criteria for Plywood Mills
Selecting an industrial veneer knife grinder requires matching machine rigidity with mill output and knife metallurgy:
1. Electromagnetic Chuck Clamping vs. Mechanical T-Slots
- ✓Electromagnetic Chuck with Digital Bevel Setting: Essential for high-capacity mills. Strong magnetic suction clamps the entire knife length instantly without mechanical clamp obstruction, preventing localized knife body bowing. Digital angle readouts allow millwrights to adjust bevels between 18° and 23° in increments of 0.1°.
- ✓Safety Demagnetization Cycle: High-end grinders feature automatic de-magnetizing cycles upon completion to prevent iron micro-dust from clinging to the blade during handling.
2. Variable-Speed Carriage Drive & Guideway Design
- ✓Linear Guide Rails vs. V-Ways: High-precision ground linear roller guide rails with central automatic forced oil lubrication provide sub-micron straightness over a 3-meter travel length.
- ✓Frequency Inverter Speed Modulation: Adjusting carriage traverse speed between 5 m/min (rough hogging pass) and 18 m/min (fine mirror finish) prevents heat concentration on thin knife tips.
3. Automatic CNC Programmable Downfeed
Modern CNC controllers (Siemens / Delta PLC) allow operators to program automated 4-stage cycles:
- 1*Rough Grinding*: Downfeed of 0.02 mm/pass to rapidly remove edge nicks and micro-chipping.
- 2*Semi-Finish Grinding*: Downfeed of 0.008 mm/pass to eliminate wheel gouge lines.
- 3*Spark-Out (Finish) Passes*: 3 to 5 zero-downfeed passes to relieve surface metallurgical stress.
- 4*Auto Retraction*: Carriage automatically returns to home position and disengages coolant.
4. High-Volume Flood Coolant & Magnetic Filtration
Overheating during grinding draws the temper from high-speed steel (HSS) or inlaid alloy cutting edges, lowering blade hardness from 60–62 HRC down to 50 HRC. A dual-sided flood coolant nozzle with a high-capacity pump and magnetic particulate separator ensures the grinding interface stays flooded, preventing thermal micro-crazing.
Preventive Maintenance & Daily Mill Inspection SOP
To guarantee razor straightness and edge longevity across an 8ft peeling knife, mill mechanics must follow a strict preventive maintenance routine:
| Inspection Frequency | Critical Checkpoints & Maintenance Actions | Target Engineering Benchmark |
|---|---|---|
| Daily Inspection (Each Shift) | • Clean electromagnetic chuck face with a non-abrasive brass scraper<br>• Measure coolant pH and synthetic concentration using a refractometer<br>• Clean magnetic chip separator drum & remove iron sludge<br>• Verify linear guide central automatic lubrication reservoir level | • Concentration: 5%–7% (Brix); pH: 8.5–9.2<br>• Chuck face: 100% free of chips & dust<br>• Lube pressure: Normal operating range |
| Weekly Maintenance | • Dress grinding cup wheel face with industrial diamond point tool<br>• Inspect carriage drive belt tension & rack-and-pinion backlash<br>• Wipe down magnetic chuck seals and inspect rubber scraper wipers | • Wheel face: Open porous grit, zero glazing<br>• Carriage backlash: < 0.02 mm<br>• Seals: Zero coolant ingress into coils |
| Monthly Precision Calibration | • Dial-indicator check: Measure chuck bed straightness along full 3100 mm stroke<br>• Verify bevel angle repeatability with digital protractor against stop blocks<br>• Flush and replace complete coolant reservoir to eliminate bacterial sludge | • Total bed runout: ≤ 0.02 mm (TIR)<br>• Bevel error: ≤ ±0.05° across full length<br>• Coolant tank: Cleaned & sterilized |
Frequently Asked Questions (FAQ)
What is the recommended knife bevel angle for peeling eucalyptus and hardwood logs?
For medium to dense hardwoods (like plantation eucalyptus, birch, and keruing), the standard primary bevel angle is between 20° and 22°. For softwoods (like radiata pine and poplar), a sharper bevel of 18° to 19° delivers smoother peel surfaces with less tear-out.
How often should a veneer peeling lathe knife be reground?
Under continuous 8-hour shift operations processing debarked logs, a high-quality alloy knife should be honed or exchanged every 4 to 8 hours. If peeling unconditioned or sandy logs, regrinding may be required every 2 to 3 hours to avoid deep nick damage.
Can one knife grinder service both 4ft and 8ft lathes?
Yes. An 8ft capacity knife grinder (e.g., Model HMD3000C) can comfortably sharpen 4ft peeling knives, clipper blades, and chipping knives. Multiple shorter knives can even be placed end-to-end on the magnetic chuck for simultaneous sharpening.
❓ Foire Aux Questions
Q:What is the recommended knife bevel angle for peeling eucalyptus and hardwood logs?
For medium to dense hardwoods, the standard primary bevel angle is between 20° and 22°. For softwoods (like radiata pine and poplar), a sharper bevel of 18° to 19° delivers smoother peel surfaces with less tear-out.
Q:How often should a veneer peeling lathe knife be reground?
Under continuous 8-hour shift operations processing debarked logs, a high-quality alloy knife should be honed or exchanged every 4 to 8 hours.
Q:Can one knife grinder service both 4ft and 8ft lathes?
Yes. An 8ft capacity knife grinder (e.g., Model HMD3000C) can comfortably sharpen 4ft peeling knives, clipper blades, and chipping knives.
Équipe d'Ingénierie Hanvy Machinery
Conçu avec plus de 30 ans d'expertise dans la fabrication de machines pour contreplaqué. Plus de 500 lignes installées dans 69 pays.
Guides Techniques Recommandés

Veneer Scarf Jointing vs. Core Composing: How to Produce Oversized & High-Strength Plywood Panels
Engineering comparison of veneer scarf jointing and core composing: 1:10 bevel geometry, longitudinal tensile strength, thermal thread composing, and machinery for container flooring and marine plywood.
Short Cycle Melamine Laminating Hot Press Machine: The Complete Industrial Guide for Plywood & Panel Mills
Industrial guide to short cycle melamine laminating presses: technical specifications, fast pre-fill hydraulics, 15-30s press cycles, thermal oil platens, and economic ROI for plywood and panel mills.
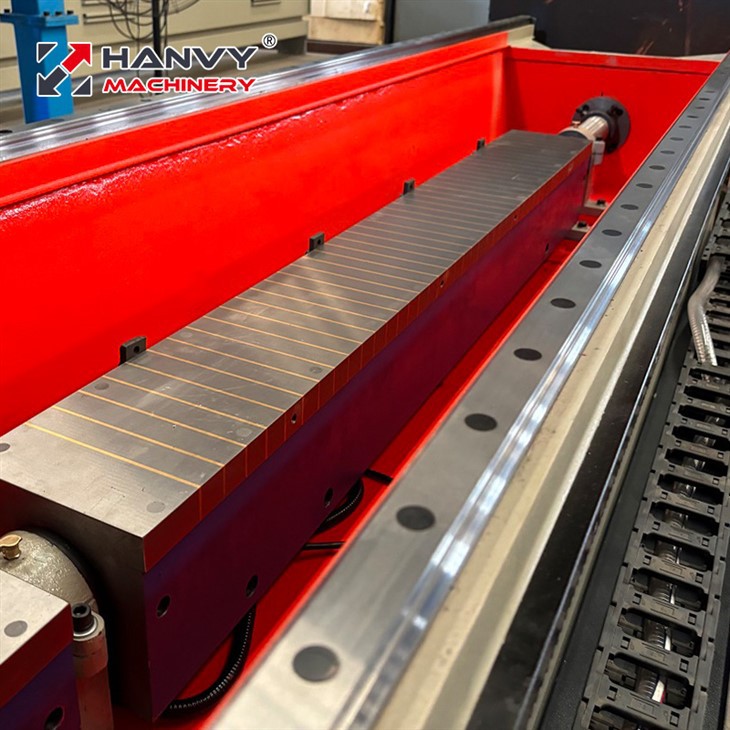
Troubleshooting Veneer Knife Grinding Defects: Edge Burning, Chatter Marks & Bowing Prevention
Engineering diagnostic guide for troubleshooting the 5 most critical veneer knife grinding failures: edge burning, chatter ripples, blade bowing, feathered burrs, and angle inconsistency.