Presses à Chaud à Fluide Thermique vs Vapeur: Efficacité Énergétique et Uniformité
Comparaison d'ingénierie entre le chauffage par fluide thermique et la vapeur pour presses à chaud. Écart de température réduit et économies d'énergie.
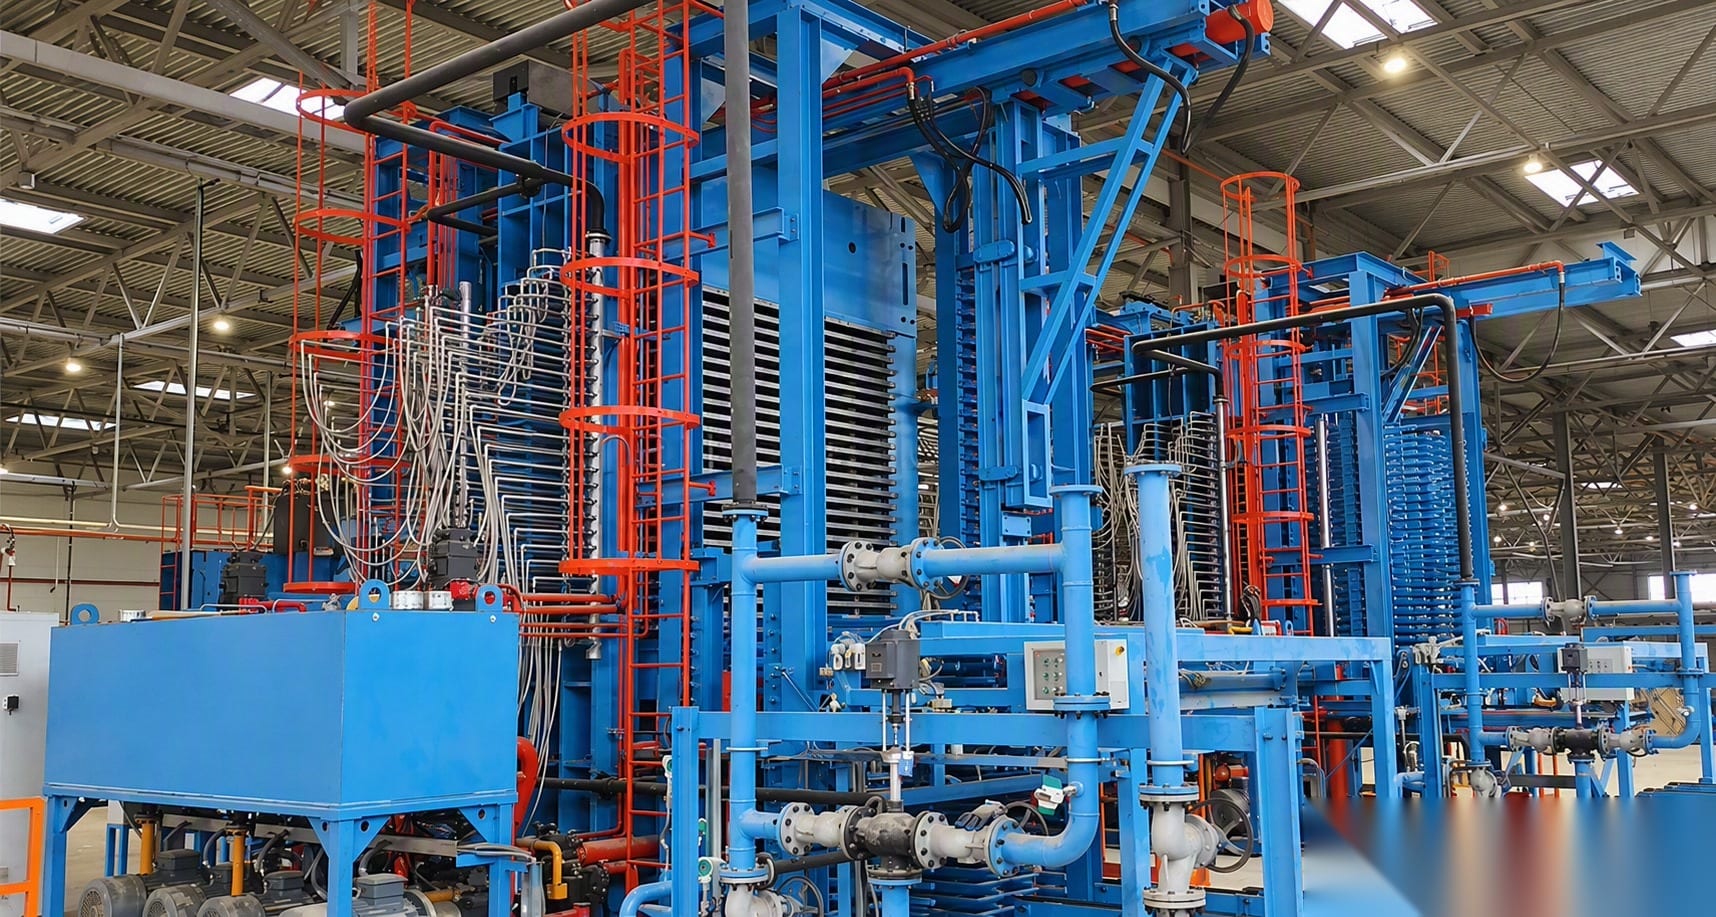
The hot press is the heart of any plywood mill. It is where adhesive polymerization occurs under high mechanical pressure and regulated heat, turning stacked glued veneers into structural panels.
When configuring a multi-layer plywood hot press, one of the most consequential decisions mill owners must make is selecting the heating medium: Thermal Oil (Hot Oil Circulation) vs. High-Pressure Steam.
This engineering guide compares thermal oil and steam systems across temperature uniformity, operating pressures, boiler safety, and lifetime operating costs to help you choose the best configuration for your plant.
1. The Core Engineering Distinction
- ✓Steam Heating Systems:
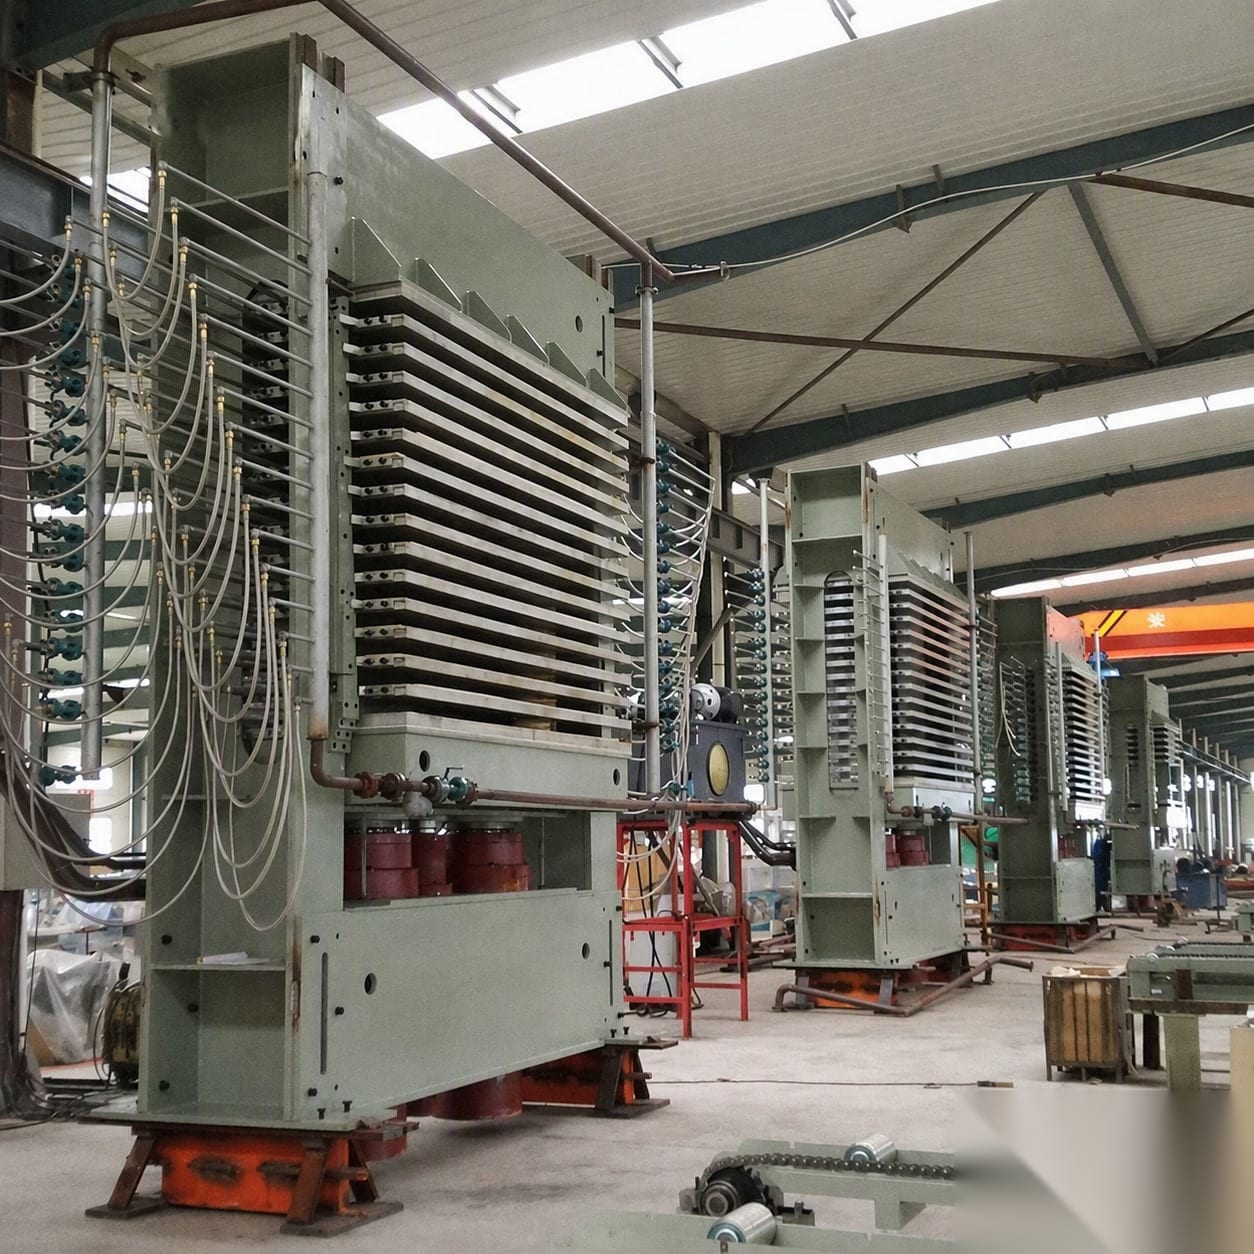
High-pressure saturated steam generated in a central boiler enters the drilled channels of the hot platens. As steam gives up its latent heat of condensation, heat transfers to the steel platen, and condensed water drains through steam traps. To achieve platen temperatures of 130 °C to 160 °C, boiler steam pressures must operate between 6 to 10 kg/cm² (bar).
- ✓Thermal Oil (Hot Oil) Systems:
A synthetic or refined mineral heat transfer oil circulates in a closed liquid loop through the platen channels. The oil is heated in a biomass- or gas-fired thermal fluid heater and pumped under low pressure (typically 2 to 4 bar). Thermal oil remains liquid at temperatures up to 300 °C without vaporizing.
2. Head-to-Head Comparison: Thermal Oil vs. Steam
| Evaluation Factor | Steam Heated Hot Press | Thermal Oil Heated Hot Press | Advantage |
|---|---|---|---|
| System Pressure | 6 – 10 bar (High pressure) | 2 – 4 bar (Low pressure) | Thermal Oil (Safer) |
| Platen Temperature Uniformity | ±4 °C to ±8 °C across platen | ±1.0 °C to ±1.5 °C | Thermal Oil (Superior) |
| Boiler Water Treatment | Required (Scale inhibitors, deaeration) | None (Closed oil loop) | Thermal Oil (Lower maintenance) |
| Corrosion & Rust Risk | Condensate causes internal pipe erosion | None (Oil lubricates channels) | Thermal Oil (Longer platen life) |
| Start-Up Heating Rate | Faster initial heat ramp-up | Slightly slower from cold start | Steam |
| Heat Recovery Efficiency | Condensate traps leak 10–15% energy | Closed loop captures 95%+ thermal return | Thermal Oil (15–20% fuel savings) |
| Max Practical Temperature | ~160 °C (requires higher boiler ratings) | Up to 220 °C+ easily | Thermal Oil (Versatile) |
3. Why Temperature Uniformity Matters for Plywood Delamination
In plywood bonding using urea-formaldehyde (UF), melamine-urea-formaldehyde (MUF), or phenol-formaldehyde (PF) resins, chemical cross-linking is sensitive to temperature:
- 1Steam Trap Air-Locks and Cold Spots:
In steam systems, platen channels frequently suffer from "condensate pooling" or steam trap failure. A platen with cold corners will fail to fully cure the glue in exterior sheet edges, resulting in board delamination, core blistering, and customer rejection.
- 1Thermal Fluid Continuous Flow:
Because thermal oil is pumped continuously in a turbulent liquid state through dual-circuit serpentine channels, there is zero phase change and zero condensate buildup. Platen surface temperature variance remains strictly within ±1.5 °C, ensuring uniform bond shear strength across every square inch of every sheet.
4. The Essential Pre-Pressing Stage: Cold Press Integration
Regardless of whether your hot press is powered by steam or thermal oil, inserting wet glued veneers directly into high-heat platens can cause steam pockets and surface blisters.
Leading plywood mills always route layed-up veneers through a heavy-duty hydraulic cold press machine prior to hot pressing. Pre-pressing for 15 to 30 minutes at room temperature allows the glue spread by the double-side glue spreader to develop initial green tack, flatten veneer ripples, and squeeze out trapped air.
For more technical parameters on platen thickness, daylight numbers, and tonnage sizing, explore our guide on how to choose the right plywood hot press machine.
5. Summary Recommendation for Modern Plywood Mills
- ✓Choose Thermal Oil If:
You are building a new plant, operating multi-opening presses (15 to 30 daylights), producing exterior-grade phenolic plywood requiring high cure temperatures (140 °C–155 °C), or prioritizing minimum boiler fuel consumption.
- ✓Choose Steam If:
Your plant already operates a high-capacity central steam boiler with spare steam capacity, or you have strict requirements for rapid initial morning start-up.
Custom Engineered Hot Presses by Hanvy Machinery
Hanvy manufactures 300T to 1200T multi-opening plywood hot press lines equipped with solid drilled Q345B steel platens, automatic hydraulic loading/unloading racks, and Siemens PLC touch-screen controls.
Équipe d'Ingénierie Hanvy Machinery
Conçu avec plus de 30 ans d'expertise dans la fabrication de machines pour contreplaqué. Plus de 500 lignes installées dans 69 pays.
Guides Techniques Recommandés

Ligne de Déroulage sans Broche: Guide de Configuration 4 ft vs. 8 ft, Rendement et Économie
Rentabilité industrielle des formats 4 et 8 pieds: calcul des économies de bois d'œuvre, intégration d'empileurs à dépression et cadences d'usine.

Séchoir à Rouleaux vs. Séchoir à Tapis: Consommation d'Énergie, Rendement et Guide de Choix
Spécifications des séchoirs Hanvy séries HG: tubes sans soudure 100 mm, roulements graphite et téflon, et réduction des consommations thermiques.
Presse Hydraulique Automatique pour Contreplaqué: Optimisation des Cycles et Courbes de Pression
Maîtrise du pressage à chaud industriel: transmission thermique au cœur du panneau, polymérisation des colles et cadences de chargement automatique.