How to Choose a Plywood Hot Press Machine: Tonnage, Layers and Heating Explained
Buying guide for plywood hot press machines: how to calculate tonnage, choose layers and openings, compare steam vs thermal oil heating, and avoid the most common mistakes.

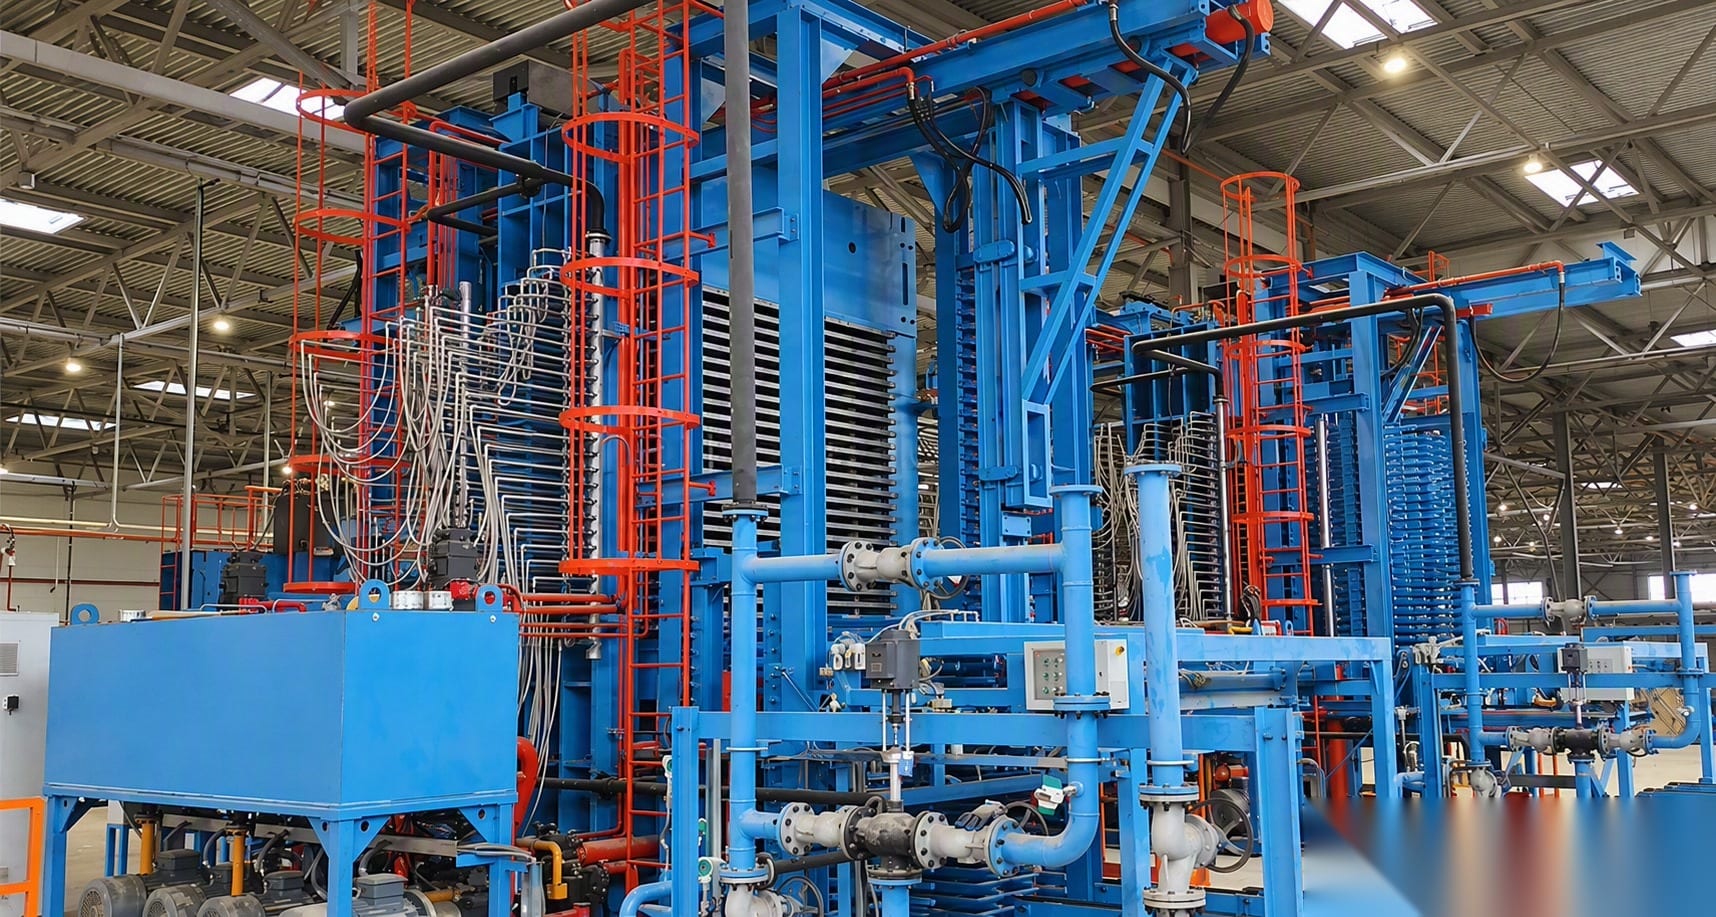
The hot press is the machine that turns glued veneer into plywood — and it is also the machine buyers choose wrong most often. Too little tonnage and the press never reaches proper bonding pressure; too few openings and your output ceiling is fixed on day one; the wrong heating system and your energy bill punishes you for years.
This guide explains the four decisions that define a plywood hot press machine: tonnage, number of openings, heating method and control/automation — with the calculations you can reuse for your own project.
Decision 1: Tonnage — Do the Pressure Math
Plywood needs roughly 15–25 kg/cm² of specific pressure during curing (varies by glue and board construction). The calculation is simple:
Specific pressure = Press tonnage ÷ Platen area
For a standard 4x8 ft platen (2700×1370 mm ≈ 36,990 cm² = 3.7 m²):
| Press capacity | Pressure on one full 4x8 panel | Verdict |
|---|---|---|
| 300 T | ~8 kg/cm² | Too low for standard plywood — film/paper lamination only |
| 400–500 T | ~11–13.5 kg/cm² | Minimum for light boards, thin constructions |
| 600 T | ~16 kg/cm² | The benchmark for 4x8 ft plywood |
| 800 T | ~21.6 kg/cm² | Comfortable margin, faster cycles, thicker boards |
| 1000–1200 T | ~27–32 kg/cm² | Heavy construction, blockboard, LVL, bamboo |
Rules of thumb that follow from this: 600T is the standard choice for normal plywood (1.5–18 mm), 800T for plants wanting margin and speed, and 1000T+ for structural boards and laminated veneer lumber. Be careful with "tonnage" claims: ask for the nominal pressure in kN and the cylinder count and diameter (for example, 2×φ380 mm main cylinders + 1×φ180 mm fast cylinder) so you can verify the calculation yourself.
Decision 2: Openings and Layers — Your Output Ceiling
Each platen gap ("opening" or "daylight") presses a batch of boards simultaneously. Output scales almost linearly with openings:
- ✓10–15 openings: small plants, ~1,500–2,500 sheets per shift
- ✓20–30 openings: mid-size plants, ~3,000–5,000 sheets per shift
- ✓35–50 openings: high-capacity automatic plants
Opening height (typically 60–100 mm) must fit your board thickness plus loading clearance. Before ordering, calculate: days/shift × boards per press × presses per hour against your target capacity — then add 20–30% headroom. Adding openings later is practically impossible; this is a one-time decision.

Decision 3: Heating Method — Steam, Thermal Oil or Electric
| Heating method | Best for | Advantages | Watch out for |
|---|---|---|---|
| Steam + boiler | Most plywood plants | Cheap, familiar technology, easy service | Boiler investment, heat loss in long pipelines |
| Thermal oil (hot oil) | Larger lines, uniform quality | Stable 100–300 °C, even platen temperature, cleaner | Oil heater investment, periodic oil checks |
| Electric | Small lines, no boiler allowed | Simple install, precise control | High electricity cost at scale |
For standard plants, steam with a coal/biomass boiler remains the most economical; thermal oil wins where board quality consistency and temperature stability matter most (furniture grade, film faced).
Decision 4: Control System, Platens and Structure
These specifications separate a durable press from a cheap one — put them in writing in your contract:
- ✓Platen material and thickness: high-strength steel Q345B, 42 mm thick for 4x8 ft presses. Ask for the steel grade certificate
- ✓Frame: welded gantry frame, frame plate thickness 30 mm+; bolted combined frames ease installation
- ✓PLC control: Siemens (or equivalent tier-brand) with touchscreen, multi-stage pressure curves and recipe storage; cheap relays-only controls cause under-cured boards
- ✓Closing speed: 8–9 m/min fast approach, then controlled slow close to avoid veneer shift
- ✓Hydraulic system: max working pressure ~25 MPa, branded pumps and valve blocks, dual pumps for fast/slow stages
Manual, Semi-Automatic or Fully Automatic?
- ✓Manual loading: lowest cost, 4–6 workers per shift on the press section, suited to low-wage markets
- ✓Semi-automatic: mechanized pushers/pullers, 2–3 workers
- ✓Fully automatic: hydraulic loading rack, press, unloading rack and stacker work as one line; 1–2 workers and consistent cycle time. Payback is typically 18–30 months on labor savings alone where wages exceed $300/month
The 5 Most Common Purchase Mistakes
- 1Buying by "layer count" alone without checking real specific pressure
- 2Accepting platens thinner than 42 mm or unstated steel grade
- 3No PLC — only relay control — then living with uneven curing
- 4Choosing openings for today's capacity with no headroom
- 5Skipping the cold press upstream, then blaming the hot press for blisters
Frequently Asked Questions
What size hot press do I need for 4x8 ft plywood?
A 600-ton press with 2700×1370 mm platens is the standard; choose 800 tons if you also press thick boards, blockboard or want faster cycles. Number of openings depends on your daily output target.
How long is one hot press cycle?
Typically 6–10 minutes per batch for 12–18 mm boards with UF glue, including loading and closing time. Thin boards cure faster; thick and exterior-grade boards slower.
Do I need both a cold press and a hot press?
For quality plywood, yes. The cold press removes air and pre-bonds the blank; without it you lose press capacity and gain blister defects.
Get a Hot Press Recommendation for Your Plant
Tell us your board size, thickness range, daily output and heating preference — we will propose the exact tonnage, openings and PLC configuration with a price, the same way we have specified presses for plants in 69 countries.
Get Hot Press Quote · WhatsApp: +86 156 1079 1577 · Email: [email protected]
❓ Frequently Asked Questions
Q:What size hot press do I need for 4x8 ft plywood?
A 600-ton press with 2700×1370 mm platens is the industry benchmark; choose 800 tons if pressing thick or high-density boards.
Hanvy Machinery Engineering Team
Engineered with 30+ years of industrial plywood machinery manufacturing expertise. Over 500 turnkey production plants installed in 69 countries worldwide.
Recommended Industry Guides

Spindleless Veneer Peeling Line: 4ft vs. 8ft Configuration Guide, Capacity & Economics
In wood veneer and plywood manufacturing, the peeling lathe is the primary profit generator of the entire mill. Every 1% improvement in green veneer recovery rate from raw round logs directly lowers the plant's cost of g...

Roller vs. Mesh Belt Veneer Dryer: Energy Cost, Output & Industrial Selection Guide
In a modern plywood factory, the veneer drying section accounts for approximately 55% to 65% of the mill's total thermal energy consumption and represents the second largest machinery capital expenditure after the peelin...
Automatic Plywood Hot Press Machine: Optimizing Pressing Cycles and Pressure Curves
In industrial plywood manufacturing, the hot pressing stage is the defining chemical and physical transformation of the process. It is here that raw wood veneers, thermosetting resin adhesive, heat, and hydraulic force c...