Comment Créer une Usine de Contreplaqué: Machines, Budget et Plan d'Atelier
Guide méthodique pour implanter une unité de production de contreplaqué: liste des machines, investissement initial, implantation d'atelier et effectifs.
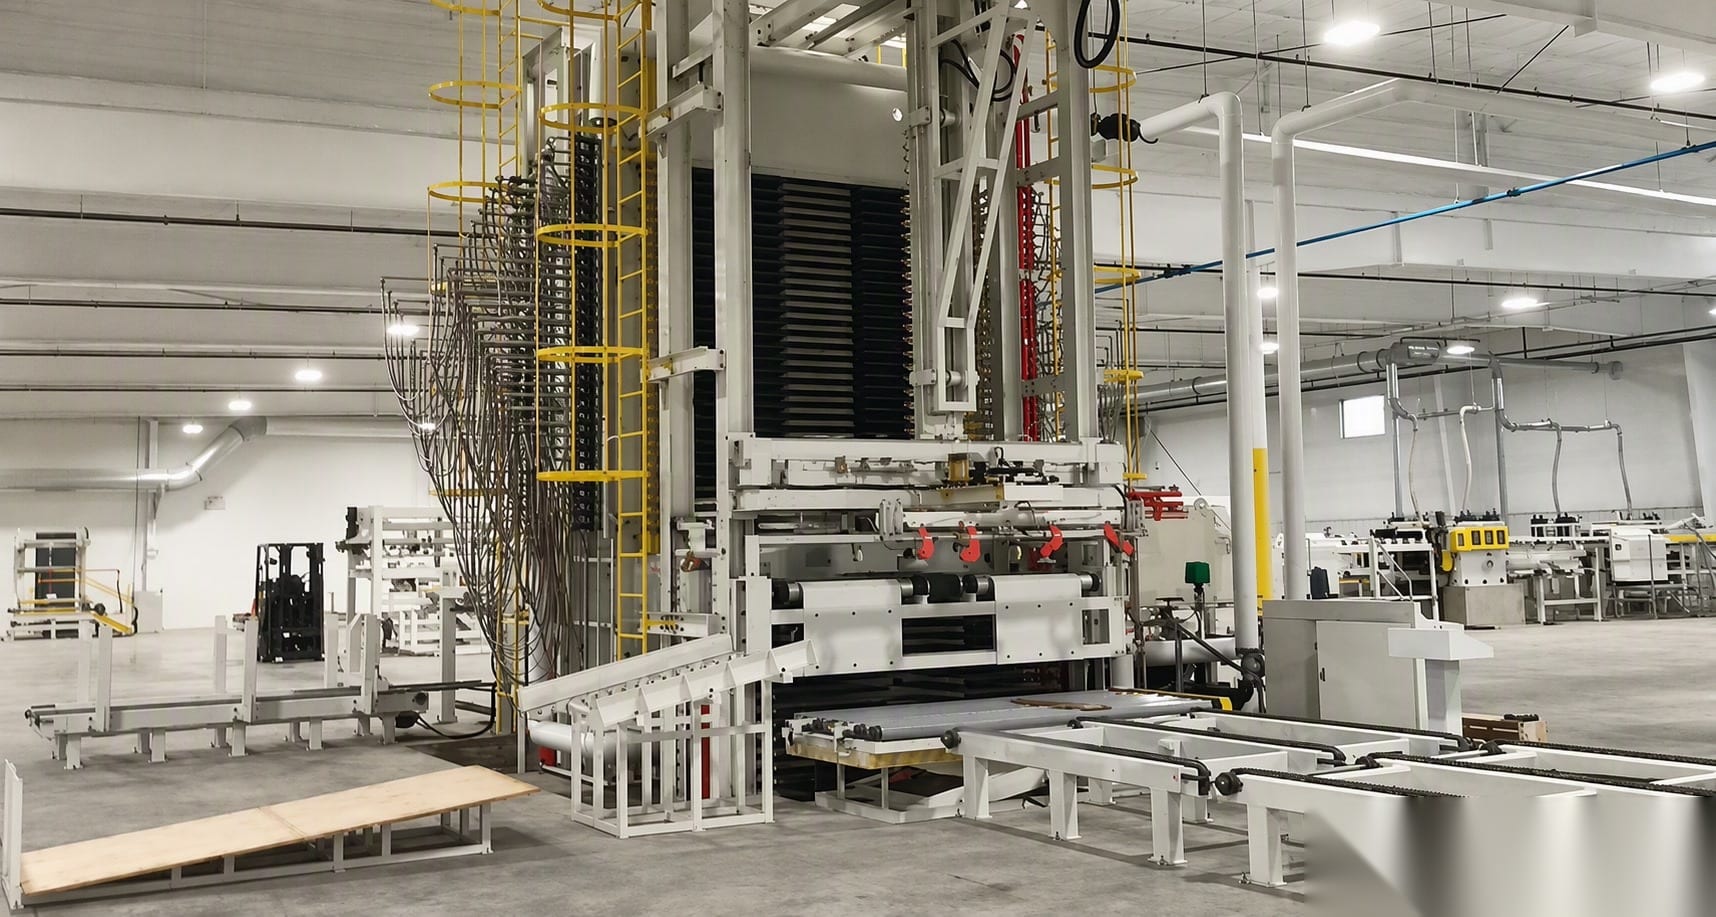
Demand for plywood keeps growing in construction, furniture and packaging markets across Southeast Asia, Africa, South America and the Middle East. That is exactly why so many investors ask the same question: how do you start a plywood factory, and what does it actually take?
This guide walks through the seven steps we use with customers in 69 countries — from defining your product to commissioning the line — with realistic budget references and the mistakes we see new owners make.

Step 1: Define Your Product and Capacity First
Everything — machine selection, budget, even the building size — flows from three decisions:
- ✓Board size: 4x8 ft (1220×2440 mm) is the global standard; some markets prefer 3x6 ft or 5x10 ft
- ✓Thickness range: most commercial plywood runs 8–18 mm; film faced and furniture grades have different face-veneer requirements
- ✓Daily capacity: small plants target 15–30 m³/day, mid-size plants 40–80 m³/day, large automatic plants exceed 100 m³/day
A useful sanity check: to produce 1 m³ of finished plywood you need roughly 2.3–2.6 m³ of logs depending on species and peeling yield, plus 8–12% glue by veneer weight. Confirm your local log supply (specie, diameter, price, seasonality) before spending anything on machines.
Step 2: Build a Realistic Investment Budget
A complete plywood manufacturing plant cost depends primarily on your intended finished product — commercial plywood, laminated/film-faced shuttering plywood, or standalone wood veneer production (see our complete Plywood Making Machine Price Breakdown for machine-by-machine figures):
1. Standard Commercial Plywood Manufacturing Plant Cost (4x8 ft)
| Plant scale | Daily capacity | Equipment budget (USD) | Core machinery setup |
|---|---|---|---|
| Small, semi-automatic | ~15–25 m³/day | 250,000 – 420,000 | 1 peeling line, 1 roller dryer, 1 manual 15-daylight hot press |
| Medium, semi-automatic | ~40–60 m³/day | 450,000 – 780,000 | 1–2 automatic peeling lines, 1 high-efficiency dryer, 1 automatic 20-daylight hot press |
| Large, fully automatic | 80–120+ m³/day | 850,000 – 1,600,000 | Dual 8ft/4ft peeling lines, continuous mesh-roller dryer, automatic loading/unloading hot press |
2. Laminated Plywood Manufacturing Plant Cost (Film-Faced Shuttering Boards)
For producing concrete formwork and phenolic film-faced plywood, you require additional secondary processing machinery:
- ✓Secondary Film Laminating Hot Press: 45,000 – 120,000 (single or multi-daylight mirror platen press)
- ✓High-Precision Edge Putty & Mending Line: 15,000 – 35,000
- ✓Automated Edge Sealing & Waterproof Spraying Booth: 12,000 – 28,000
- ✓Total Laminated Plywood Plant Surcharge: Typically +90,000 to 220,000 above raw commercial plant budget, yielding 35–50% higher finished board profit margins in construction markets.
3. Standalone Wood Veneer Production Plant Cost (Peeling & Drying Station)
If your local timber concession is abundant but downstream panel market is regional, setting up a veneer-only plant requires lower initial capital:
| Veneer plant scale | Target output | Equipment budget (USD) | Core equipment |
|---|---|---|---|
| Small veneer peeling unit | 20–30 m³ logs/day | 60,000 – 110,000 | Hydraulic debarker + 4ft/8ft spindleless peeling lathe + auto rotary clipper |
| Complete veneer mill with drying | 60–100 m³ logs/day | 180,000 – 360,000 | Debarker + peeling line + 4-deck roller or breathing hot press veneer dryer |
Add 20–35% for international ocean freight, on-site commissioning engineers, industrial thermal oil boiler, civil concrete foundations and initial spare parts on top of equipment cost. Keep at least two months of wages and log purchases as operational working capital.
Step 3: Know the Machine Checklist by Heart
A working plywood factory needs these stations in order:
- 1Log cutting saw – cross-cuts logs to peeling length
- 2Log debarker / rounder – removes bark and rounds the log before peeling
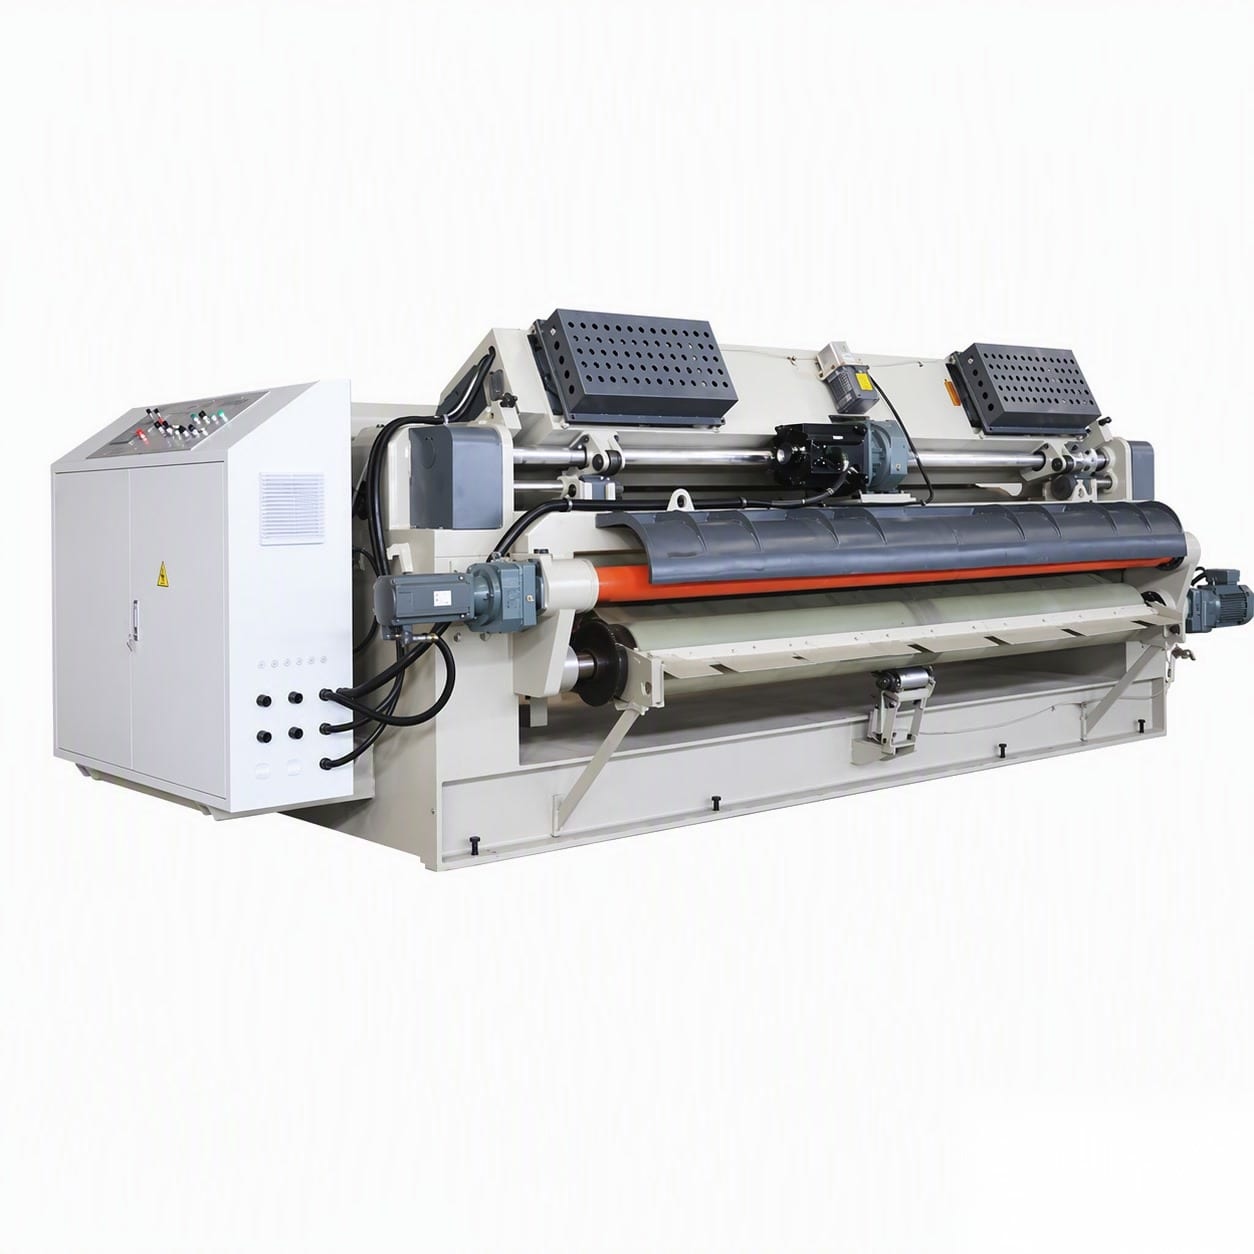
- 3Veneer peeling machine – the heart of the plant; spindleless machines peel cores down to a 40 mm leftover, spindle lathes produce face veneer
- 4Veneer dryer – roller or mesh type, sized by the number of heating sections
- 5Glue spreader – single or double side glue applicator
- 6Core veneer composer / lay-up line – builds the board blank
- 7Cold press / pre-press – pre-compacts the blank and removes air
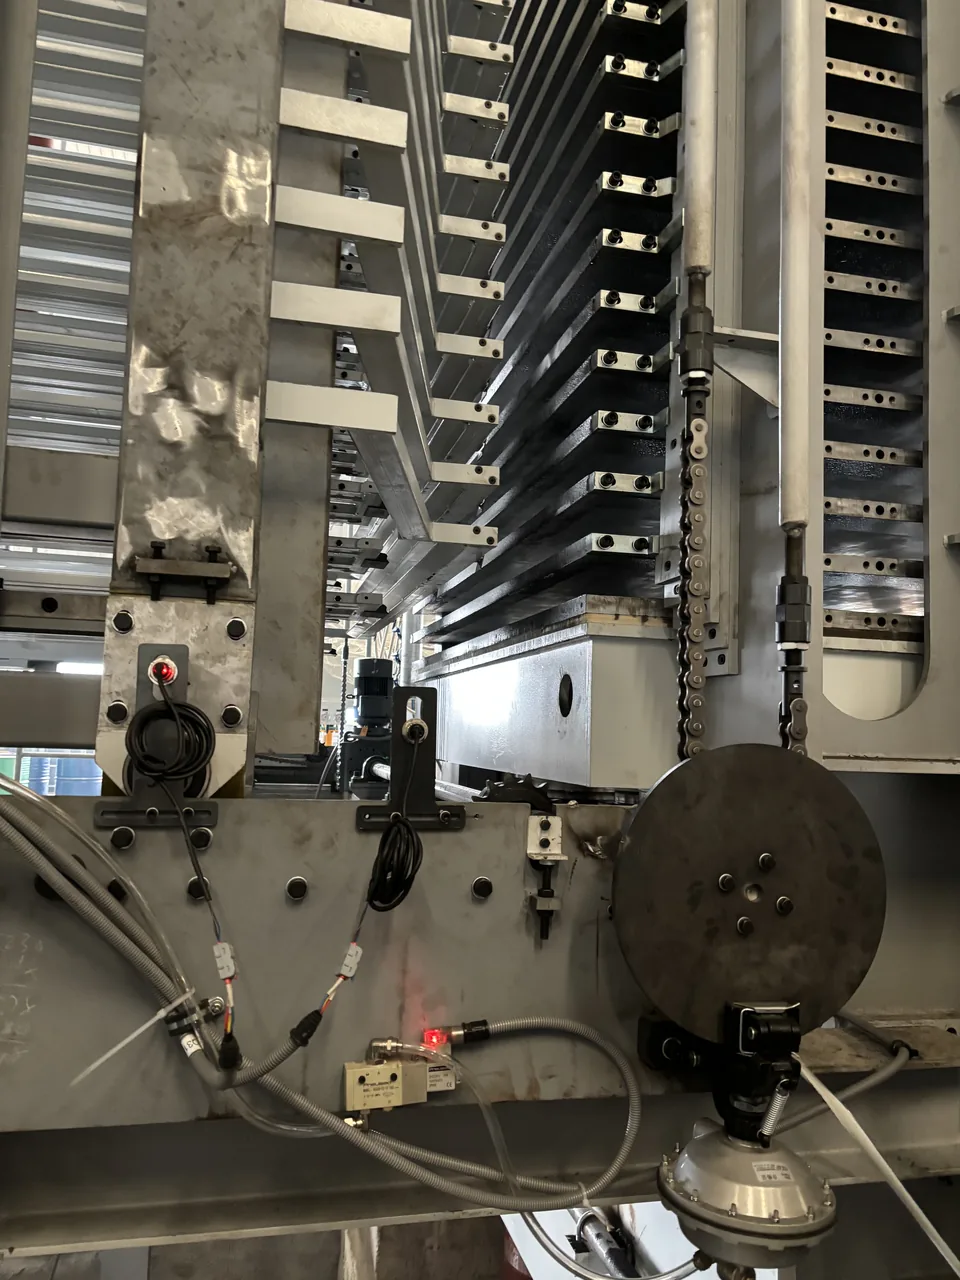
- 8Hot press – cures the panel under hydraulic heat and pressure (read our hot press selection guide)
- 9Edge trimming saw (double side / DD saw) – cuts to final panel dimension
- 10Wide belt sanding machine – calibration and surface polishing
Optional stations include a putty/mending line, film faced laminating press, moisture sorting and automatic packing. Buy the hot press and dryer slightly above today's need — these two machines define your ceiling. For complete turnkey integration, explore our Turnkey Plywood Production Line Solutions.
Step 4: Site, Building and Layout
Rule of thumb for space:
- ✓Land: 8,000–15,000 m² for a mid-size plant, including a covered log yard
- ✓Production hall: at least 2,500–4,000 m², with 6–8 m clear height under the roof for the dryer and hot press structures
- ✓Power: 500–1,000 kVA installed capacity for a mid-size automatic line; confirm voltage/frequency with suppliers early (380V/50Hz is the machinery standard)
- ✓Water & drainage: for the boiler and glue room
- ✓Log yard flow: trucks should enter, dump and exit without reversing through production traffic
Lay the line in a straight flow — log yard → cutting → peeling → drying → gluing/lay-up → pressing → trimming → sanding → packing — so boards never travel backwards. A good supplier will draw the layout for you from your building dimensions; insist on this service before ordering.
Step 5: Secure Raw Material and Glue
- ✓Logs: sign seasonal supply agreements; mixed eucalyptus and pine is common in tropical plants, poplar and birch in continental climates
- ✓Glue: urea-formaldehyde (UF) for interior grades, phenol-formaldehyde (PF) or melamine-modified for exterior/film faced grades; budget a small glue mixing station rather than buying pre-mixed
- ✓Face veneer: if you cannot peel quality faces from local logs, plan a face-veneer purchase budget
Step 6: Staffing
A semi-automatic 4x8 ft line typically runs with 8–12 workers per shift (peeling line 3–4, dryer/glue 2–3, press 2–3, trimming/sanding 2, plus a maintenance electrician and fitter). Full automation cuts this to 3–5 per shift but demands better-trained technicians. Plan the supervisor's visit to your supplier's factory during installation — free training on real machines is worth more than any manual.
Step 7: Order, Install and Commission
A typical timeline from contract to first sale:
- 1Contract and layout drawings – 2 weeks
- 2Machine manufacturing – 30–60 days
- 3Ocean freight – 3–6 weeks depending on destination
- 4Civil works and power readiness – parallel with shipping
- 5Installation and commissioning – 20–45 days with the supplier's engineers
- 6Ramp-up – 2–4 weeks to reach rated output
Common Mistakes New Plywood Factory Owners Make
- ✓Buying the cheapest hot press (thin platens, weak hydraulics) and living with 30% lower output forever
- ✓Matching the veneer dryer to today's capacity instead of tomorrow's — the dryer is the plant's bottleneck
- ✓Skipping the cold press to save money, then fighting blistered boards in the hot press
- ✓No spare peeling knives, saw blades or seals on site when the first breakdown happens
- ✓Ordering machines before finalizing the building layout (consult our 7-step manufacturing process guide)
Frequently Asked Questions
How much land do I need for a plywood factory?
For a mid-size 4x8 ft plant producing ~50 m³/day, plan 8,000–15,000 m² total including log yard, production hall of 2,500–4,000 m² and packing/storage areas.
How long does it take to start producing?
From contract to first sellable boards usually takes 4–6 months, assuming the building and power are ready when machines arrive.
Can I start with just one machine?
You can start a veneer-selling business with a veneer peeling line only, but producing plywood requires at least the peeling–pressing–trimming chain described above.
Ready to Plan Your Plywood Factory?
Send us your target board size, daily capacity, log species and building dimensions. Our engineers will design the machine list and factory layout for free — the same process we have used for 500+ turnkey projects in 69 countries.
Équipe d'Ingénierie Hanvy Machinery
Conçu avec plus de 30 ans d'expertise dans la fabrication de machines pour contreplaqué. Plus de 500 lignes installées dans 69 pays.
Guides Techniques Recommandés

Ligne de Déroulage sans Broche: Guide de Configuration 4 ft vs. 8 ft, Rendement et Économie
Rentabilité industrielle des formats 4 et 8 pieds: calcul des économies de bois d'œuvre, intégration d'empileurs à dépression et cadences d'usine.

Séchoir à Rouleaux vs. Séchoir à Tapis: Consommation d'Énergie, Rendement et Guide de Choix
Spécifications des séchoirs Hanvy séries HG: tubes sans soudure 100 mm, roulements graphite et téflon, et réduction des consommations thermiques.
Presse Hydraulique Automatique pour Contreplaqué: Optimisation des Cycles et Courbes de Pression
Maîtrise du pressage à chaud industriel: transmission thermique au cœur du panneau, polymérisation des colles et cadences de chargement automatique.