Cómo Elegir el Torno sin Husillo Adecuado para Chapa Interior vs. Chapa Facial
Guía técnica para configurar tornos desenrolladores CNC para chapa gruesa de núcleo frente a chapa delgada de cara con acabado liso de alta calidad.
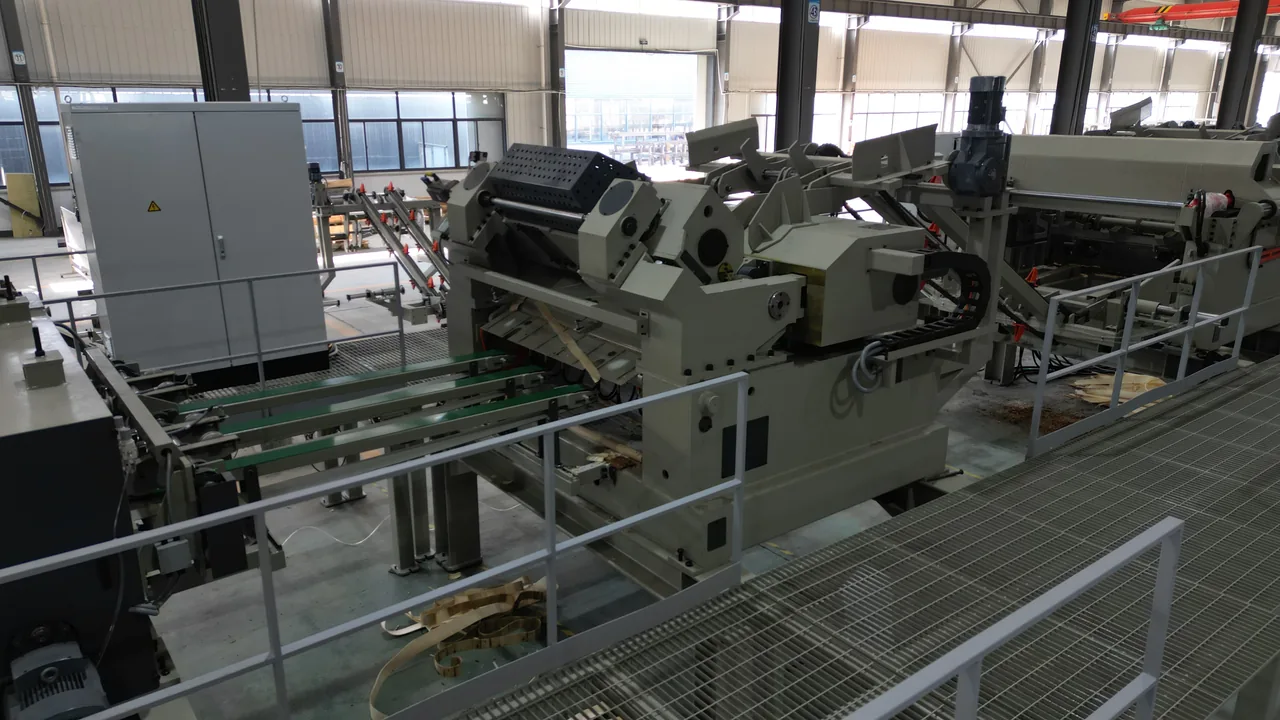
In rotary veneer peeling, one of the most critical machine specification decisions an investor or mill manager must make is whether a lathe is optimized for heavy structural core veneer or high-finish decorative face veneer.
While modern CNC spindleless veneer peeling lathes provide remarkable versatility, the mechanical requirements for peeling a 2.6 mm thick eucalyptus core sheet at 80 m/min are fundamentally different from peeling a 0.35 mm ultra-thin birch or poplar face sheet with zero surface lathe checks.
Attempting to run thin face veneers on a coarse core lathe leads to torn fibers, uneven thickness ribbons, and frequent knife chattering. Conversely, running heavy core veneers on an under-powered face lathe strains servo ball screws and risks roller stalling.
This engineering guide details the technical specifications, knife geometry, roller configurations, and servo drive systems required to select the right spindleless lathe for your production goals.
1. The Engineering Trade-Off: Peeling Physics of Core vs. Face
| Peeling Parameter | Core Veneer Application | Face / Surface Veneer Application |
|---|---|---|
| Typical Thickness | 1.5 mm – 3.6 mm | 0.25 mm – 0.8 mm |
| Priority Metric | Volume throughput (m³/hour), residual core size | Surface smoothness, thickness consistency (±0.02 mm) |
| Cutting Speed | High speed: 60 – 90 m/min | Moderate speed: 35 – 55 m/min |
| Cutting Force / Resistance | Very high (requires massive machine mass) | Moderate (requires micro-step precision) |
| Acceptable Lathe Checks | Moderate allowable micro-checking | Near-zero checks; tightly compressed wood fibers |
| Knife Bevel Angle | 20° – 22° (sturdy, impact-resistant) | 17° – 19° (razor sharp, low cutting resistance) |
| Pressure Bar Design | Heavy fixed or driven nosebar | Micro-adjustable precision roller nosebar |
2. Machine Architecture Differences: What to Look for in the Specs
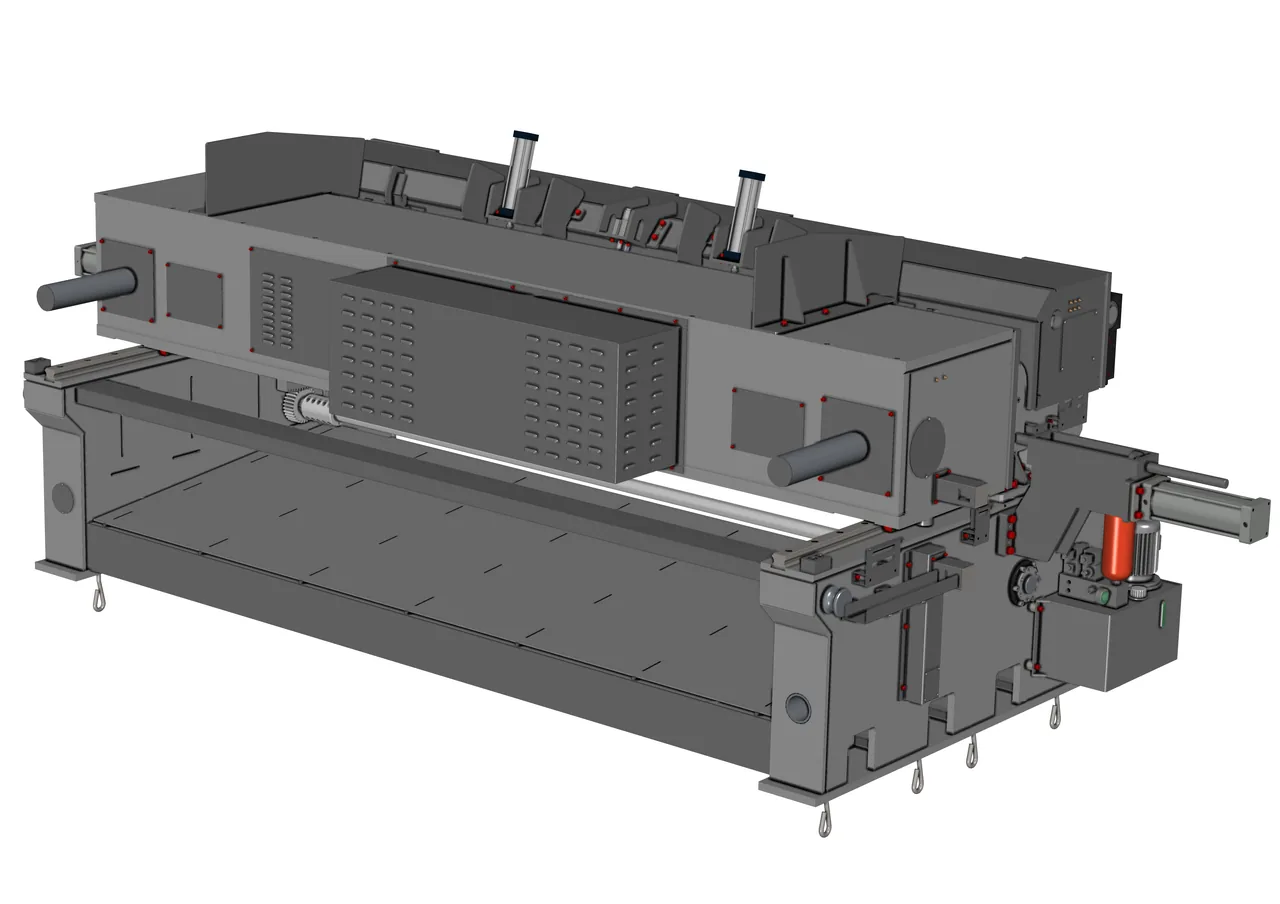
1. Roller Diameter and Knurling Profile
- ✓For Core Veneer:
Requires large-diameter driving rollers (typically 125 mm to 140 mm) with aggressive CNC spiral or diamond knurling. This delivers the immense rotational torque needed to drive the log through deep knife engagements without slipping.
- ✓For Face Veneer:
Rollers must feature precision fine-pitch knurling or specialized induction-hardened micro-teeth. Aggressive teeth will indent or bruise thin face veneer as it rolls off the knife edge, creating visible pattern marks after sanding.
2. Servo Feed Drive and Ball Screw Rating
- ✓For Core Veneer:
Heavy pitch ball screws (e.g., 50 mm diameter, 10 mm lead) coupled with high-torque servo motors (7.5 kW – 11 kW) to handle rapid tool advances and severe resistance spikes when hitting hard timber knots.
- ✓For Face Veneer:
High-resolution absolute encoders (23-bit or optical linear scale feedback) are mandatory. The servo system must execute micro-infeeds as fine as 0.005 mm per rotation with zero backlash.
3. Automatic Hydraulic Gap Regulation
As a log's diameter slims down, cutting resistance vectors shift. High-tier Hanvy lathes incorporate CNC proportional gap control: the machine automatically adjusts the vertical gap and horizontal clearance between the knife edge and pressure bar in real-time according to peeled thickness and instantaneous log diameter.
3. Upstream Preparation: Why Log Rounding Determines Face Quality
High-quality face veneer cannot be peeled from an out-of-round log. Before presenting timber to a face lathe:
- 1Logs must be processed through an automatic hydraulic log debarker to strip all abrasive bark, soil, and grit.
- 2The log must be centered optically to align the true geometric grain with the lathe axis, ensuring concentric annular growth rings.
- 3For dense hardwoods (e.g., birch, eucalyptus, keruing), logs should be pre-conditioned in hot water vats (60°C) to soften lignin, allowing the blade to produce smooth, non-fuzzy face veneer sheets.
4. Downstream Integration: Continuous Peeling-Clipping-Stacking Lines
In a modern high-recovery mill, the spindleless lathe does not operate in isolation:
- ✓Synchronized Rotary Clipper:
A high-speed pneumatic rotary clipper cuts the continuous veneer ribbon into standard 4x8 ft (1300x2600 mm) sheets at line speeds exceeding 70 m/min, cutting out defects via optical camera sensors.
- ✓Vacuum Sheet Stacker:
Diverts full-size face sheets and partial core strips into separate bins, preventing sheet wrinkling and edge tears caused by manual stacking.
- ✓Direct Transfer to Jet Dryer:
Sheets feed directly into your multi-deck continuous veneer dryer to lock in moisture content between 8% and 12%.
5. Frequently Asked Questions (FAQ)
Can one spindleless lathe peel BOTH face and core veneer?
Yes, with a dual-mode CNC recipe controller. Hanvy CNC spindleless lathes allow operators to store distinct parameter profiles for face veneer (0.3–0.6 mm, slow feed, fine nosebar gap) and core veneer (1.5–3.2 mm, high speed, wide nosebar gap), switching recipes on the touchscreen in seconds.
How small of a core can Hanvy spindleless lathes achieve?
Hanvy lathes consistently peel logs down to a residual core diameter of 25 mm to 30 mm (pencil-thin core), yielding up to 82% theoretical wood recovery from small plantation logs.
Configure Your Custom Peeling Line
Whether your mill prioritizes maximum volume output for structural plywood or razor-sharp accuracy for decorative hardwood face panels, Hanvy engineers will tailor lathe motor ratings, roller diameters, and knife assemblies to your timber species.
Equipo de Ingeniería de Hanvy Machinery
Diseñado con más de 30 años de experiencia en maquinaria para contrachapado. Más de 500 plantas llave en mano instaladas en 69 países.
Guías Industriales Recomendadas

Línea de Desenrollo de Chapa sin Husillo: Comparativa 4 ft vs. 8 ft, Capacidad y Rentabilidad
Análisis económico y productivo para tornos de chapa de 4 y 8 pies: ahorro de hasta $990 por turno en madera y configuración de líneas continuas.

Secador de Rodillos vs. Malla: Costos Energéticos, Producción y Guía de Selección
Especificaciones y ventajas mecánicas de secadores Hanvy: rodillos sin costura de 100 mm, cojinetes de PTFE autolubricados y rendimiento por metro cúbico.
Prensa Hidráulica Automática de Contrachapado: Optimización de Ciclos y Curvas de Presión
Control avanzado de prensado en caliente: etapas de compresión, respiración para escape de vapor y garantía de resistencia mecánica según normas EN/ASTM.