Proceso de Fabricación de Contrachapado: 7 Pasos desde el Tronco hasta el Tablero Terminado
Cómo se fabrica el contrachapado: el proceso completo de 7 etapas desde el corte de trozas hasta el lijado final, con mermas típicas y puntos de control de calidad.

Plywood looks simple — thin sheets of wood glued together — but turning a rough log into a stable, square, sandable panel is a chain of seven connected processes, and a mistake in any one of them shows up in the final board.
Whether you are setting up a new plant or buying equipment for an existing one, understanding the plywood manufacturing process step by step is the fastest way to know which machines matter and where the money is lost.

The 7 Steps at a Glance
| # | Step | Machine | Typical loss |
|---|---|---|---|
| 1 | Log cutting | Log cutting saw | 3–10% |
| 2 | Debarking & rounding | Log debarker / rounder | 2–5% |
| 3 | Veneer peeling | Veneer peeling machine | 5–10% (plus the core leftover) |
| 4 | Veneer drying | Veneer dryer | 4–10% (shrinkage) |
| 5 | Gluing & composing | Glue spreader + composer | 4–16% |
| 6 | Pressing (cold + hot) | Cold press + hot press | 3–8% |
| 7 | Trimming & sanding | Edge saw + sanding machine | 8–15% |
End-to-end, a well-run plant converts roughly 40–45% of incoming log volume into saleable plywood; the rest becomes core leftovers, trim, bark and dust — much of which can be sold as biomass fuel or used to fire the boiler.
Step 1–3: From Log to Veneer
Log cutting. Import logs arrive 6+ meters long and are cross-cut to peeling length — usually the product length plus a small allowance (e.g. 1220×2440 mm boards are peeled from 2600 mm or 1300 mm log sections). Straight, well-stored logs cut cleanly; curved or rotten sections raise waste fast.
Debarking and rounding. A hydraulic debarker strips the bark and rounds the log so the peeling knife meets a true cylinder. Skipping this step is the most common cause of broken veneer and knife damage.
Veneer peeling. The peeling machine rotates the log against a long knife and unrolls it into a continuous ribbon of veneer. Core veneer (1.6–2.2 mm) comes from high-speed spindleless machines that peel the log down to a 40 mm core; face veneer (0.3–0.8 mm) is peeled on precision spindle lathes. Peeling thickness accuracy here decides the flatness of the final board.

Step 4–5: Drying, Gluing and Composing
Drying. Fresh veneer carries 60–100% moisture and must be dried to 8–12% before gluing. Roller dryers suit thick core veneer; mesh dryers handle thin face veneer gently. Under-dried veneer blisters in the hot press; over-dried veneer cracks and absorbs too much glue.
Gluing and composing. Veneer passes through a glue spreader (single- or double-side), then layers are laid up cross-grain: face / core / core / back. Automatic composer lines replace the slow manual stacking that still dominates small factories, cutting labor and fixing layer alignment.
Step 6: Pressing — Where the Panel Is Born
Cold press first. The glued blank goes into a cold press that pre-compacts it at room temperature and squeezes out air. This shortens the hot press cycle and prevents blisters.
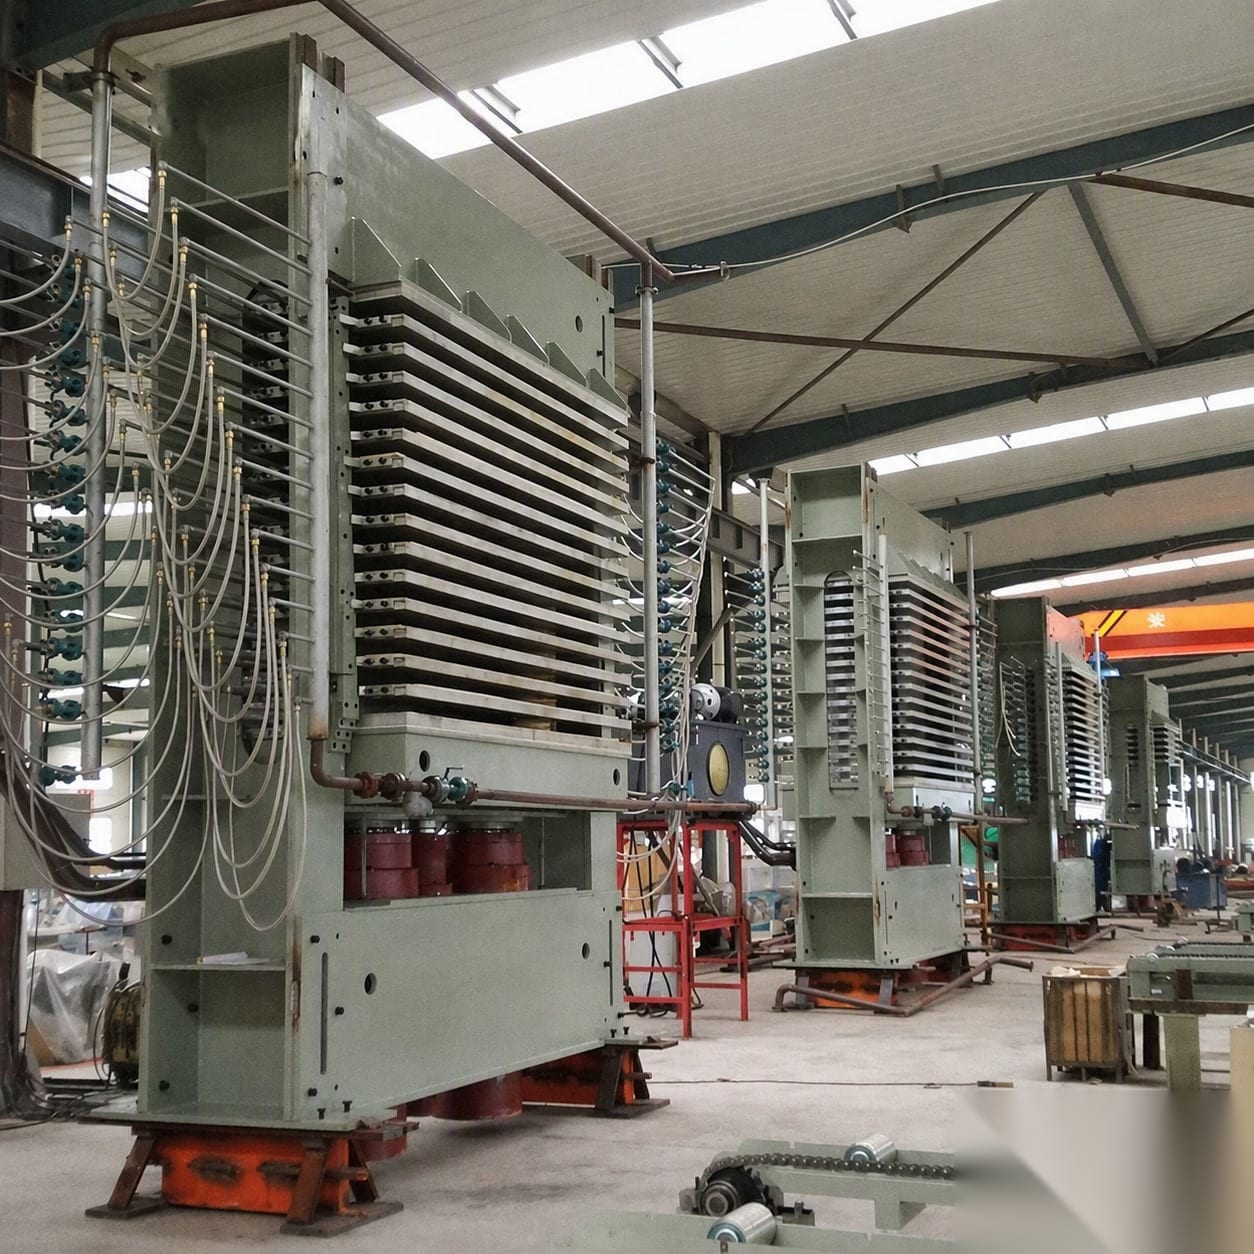
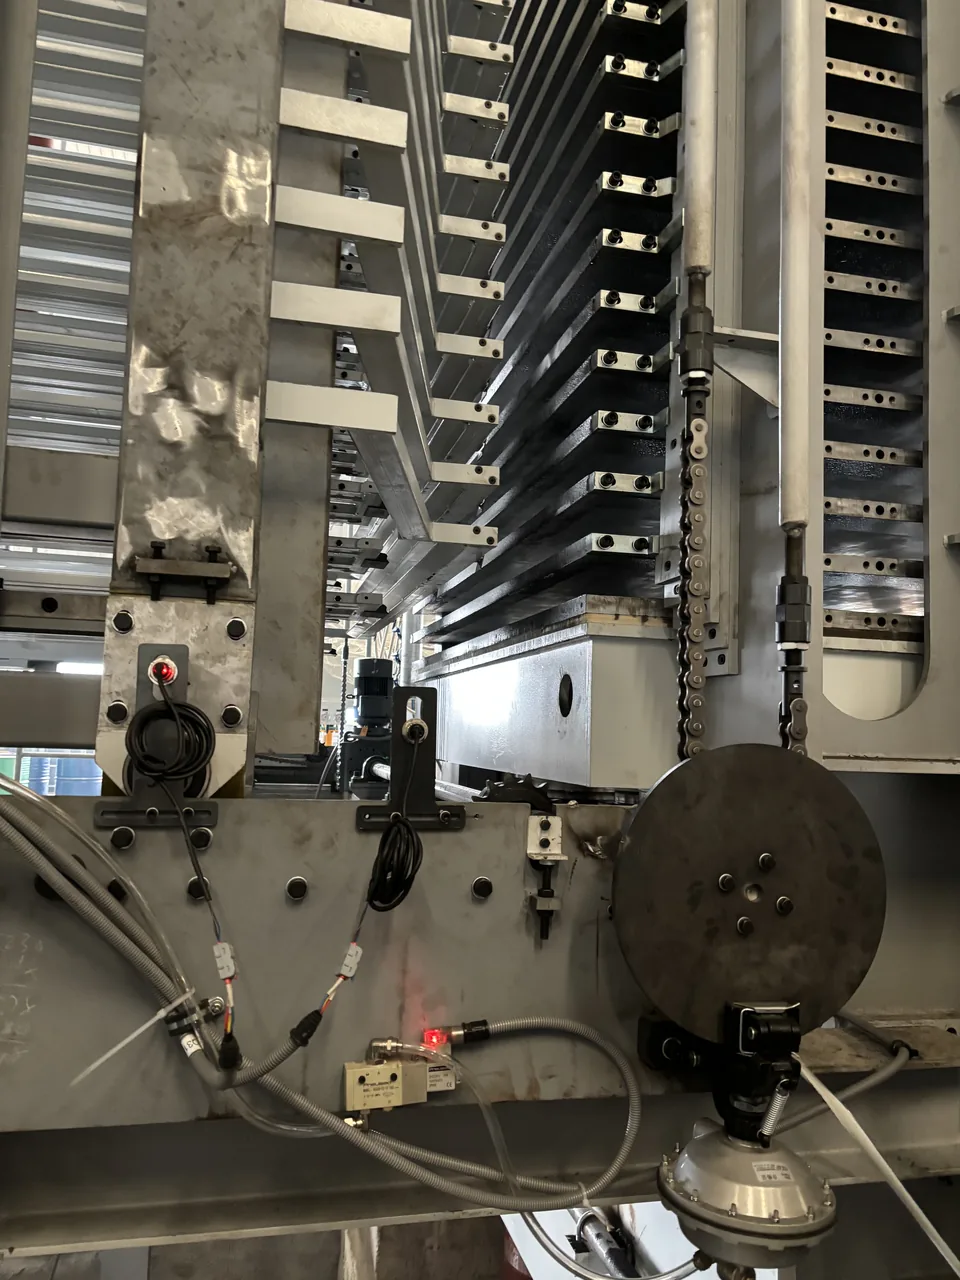
Hot press cures the glue. The panel then enters the multi-daylight hot press, where heated platens (steam or thermal oil, typically 100–130 °C for UF glue) cure the resin under 15–25 kg/cm². Cycle time depends on thickness: roughly 1 minute per mm of board thickness is a common starting point. Pressure control, platen flatness and even heating decide whether the board comes out solid or delaminated.
Step 7: Trimming and Sanding
Edge trimming. A double-side (DD) saw trims the pressed panel to exact final dimensions — for example from an oversized blank to a square 1220×2440 mm board. Modern automatic saws cut 3,000–4,000 sheets per shift with two workers.
Sanding. A wide belt sander calibrates thickness to tolerance and smooths the surface for grading, film lamination or direct sale. Panels are then inspected, graded, stacked and packed.
Quality Checkpoints That Separate Good Plants from Average Ones
- 1Measure veneer thickness across the ribbon every hour — drift here multiplies through the whole stack
- 2Check dried veneer moisture with a meter, not by feel (target 8–12%)
- 3Control glue coverage in g/m² by weighing sample sheets before and after spreading
- 4Verify hot press platen temperature uniformity with an infrared thermometer weekly
- 5Test board bonding quality daily (boil or soak samples for exterior grades)
- 6Keep a sample board from every shift with date and parameters written on it
Frequently Asked Questions
How long does the plywood manufacturing process take?
From log infeed to finished board, material moves through the line in 2–4 hours including drying time; actual press curing takes minutes per batch. Throughput is set by the slowest station — usually peeling or the hot press.
How many logs does one cubic meter of plywood need?
Typically 2.3–2.6 m³ of logs per 1 m³ of finished plywood, depending on species, log diameter and peeling efficiency.
What is the most energy-intensive step?
Veneer drying and hot press heating together account for most thermal energy demand, which is why efficient dryers with heat recovery matter so much for operating cost.
Want to See the Process on a Real Line Layout?
We can provide a detailed process flow drawing matched to your building and capacity, with machine specifications for every station of the plywood manufacturing process.
Request a Process Layout · WhatsApp: +86 156 1079 1577 · Email: [email protected]
❓ Preguntas Frecuentes
Q:How long does the plywood manufacturing process take?
From log infeed to finished board, material moves through the line in 2–4 hours including drying time; actual press curing takes minutes per batch.
Equipo de Ingeniería de Hanvy Machinery
Diseñado con más de 30 años de experiencia en maquinaria para contrachapado. Más de 500 plantas llave en mano instaladas en 69 países.
Guías Industriales Recomendadas

Línea de Desenrollo de Chapa sin Husillo: Comparativa 4 ft vs. 8 ft, Capacidad y Rentabilidad
Análisis económico y productivo para tornos de chapa de 4 y 8 pies: ahorro de hasta $990 por turno en madera y configuración de líneas continuas.

Secador de Rodillos vs. Malla: Costos Energéticos, Producción y Guía de Selección
Especificaciones y ventajas mecánicas de secadores Hanvy: rodillos sin costura de 100 mm, cojinetes de PTFE autolubricados y rendimiento por metro cúbico.
Prensa Hidráulica Automática de Contrachapado: Optimización de Ciclos y Curvas de Presión
Control avanzado de prensado en caliente: etapas de compresión, respiración para escape de vapor y garantía de resistencia mecánica según normas EN/ASTM.