Factores Clave en la Eficiencia del Descortezado Hidráulico y Rendimiento de Trozas
Guía técnica para maximizar el aprovechamiento de trozas, velocidad de cilindrado y vida útil de cuchillas mediante descortezadoras hidráulicas pesadas.
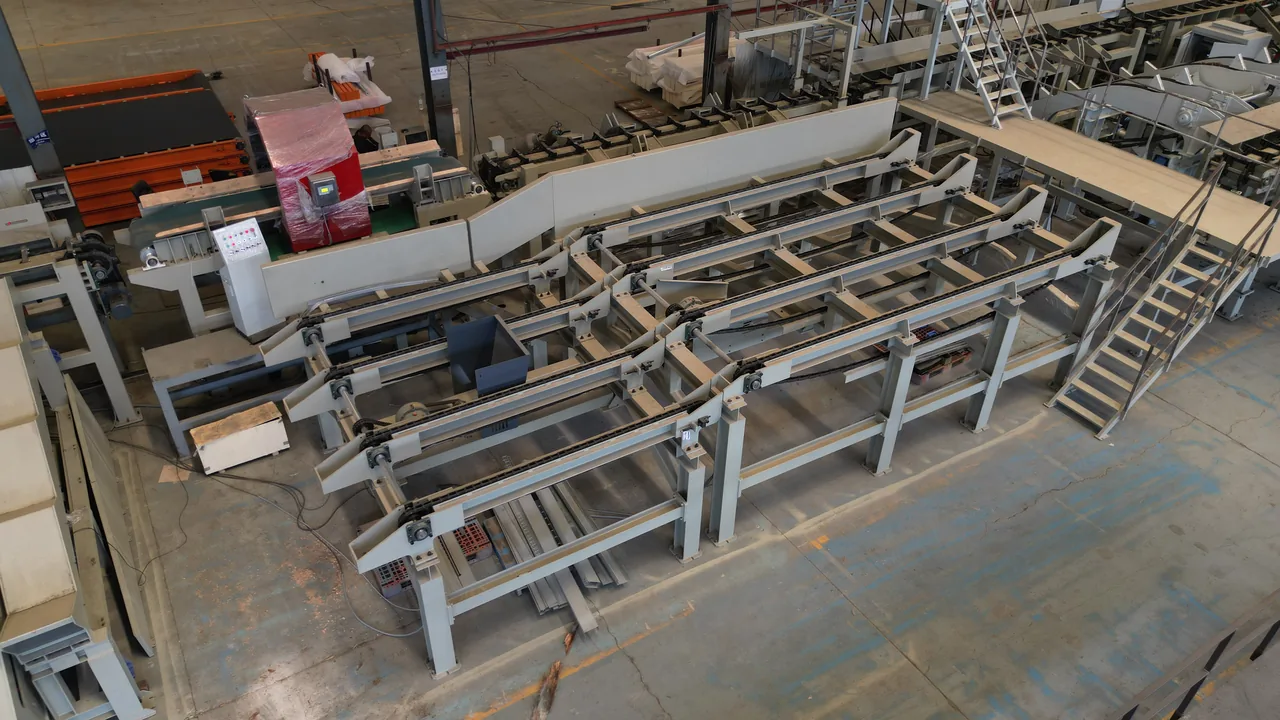
In commercial rotary veneer and plywood production, the hydraulic log debarker is the primary gatekeeper for the entire mill. Every log entering the plant must first be stripped of its abrasive bark, cleared of embedded stones and sand, and rounded from an irregular, tapered natural shape into a true geometric cylinder.
Any inefficiency or dimensional error introduced at the debarking station propagates catastrophically downstream:
- ✓Incomplete debarking introduces grit and silica that instantly destroys expensive knife edges on your spindleless veneer peeling lathe.
- ✓Excessive cutting into white wood wastes valuable timber volume, shrinking whole-log recovery by 5% to 12%.
- ✓Slow debarker cycle times starve downstream peeling lines, capping whole-plant daily output.
This engineering guide examines the mechanical, hydraulic, and operational factors that govern hydraulic log debarker efficiency, and how modern dual-roller machines maximize timber recovery.
1. Mechanical Mechanisms: Dual Roller Traction vs. Hydraulic Cutterhead
A high-performance hydraulic log debarker operates through two coordinated mechanical subsystems:
Heavy-Duty Knurled Drive Rollers
- ✓Friction Traction:
Two large-diameter, hardened alloy steel rollers (one driven roller and one idle/driven tracking roller) cradle the rotating log from beneath.
- ✓Self-Cleaning Tooth Profile:
Traction teeth are CNC-machined into the roller surfaces to bite through thick fibrous bark (such as pine or eucalyptus) without slipping, even on wet, frozen, or resinous logs.
Hydraulic Floating Cutterhead
- ✓Dual Hydraulic Cylinders:
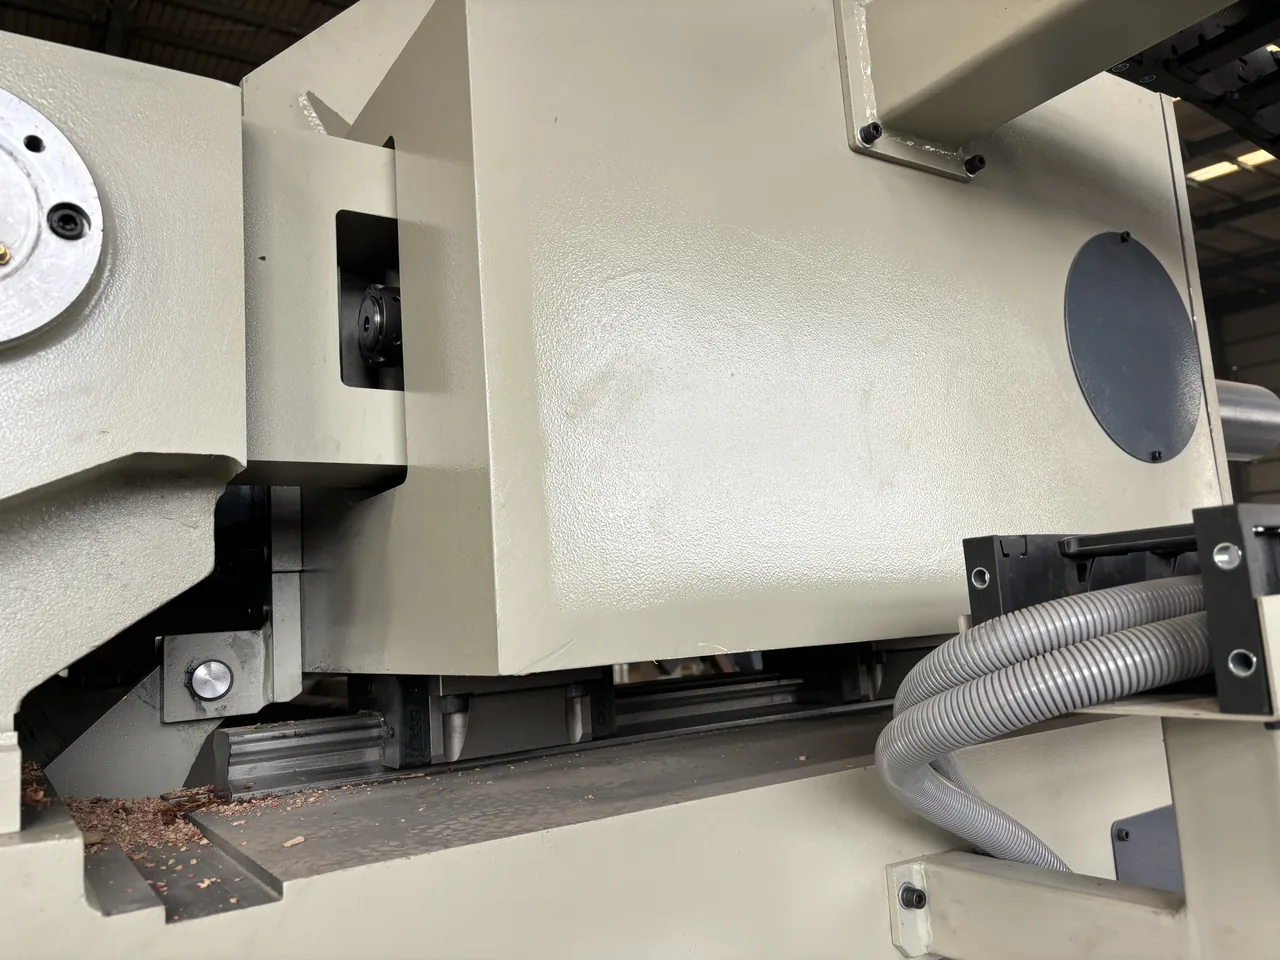
The debarking and rounding knife carriage is pressed downward against the log by heavy hydraulic cylinders controlled via proportional relief valves.
- ✓Tension and Contour Tracking:
The hydraulic pressure must be stiff enough to shave irregular tree knots and oval bulges rapidly, yet compliant enough to follow the natural longitudinal taper of the log without gouging deep into prime outer timber.
2. The Critical Role of Debarking in Veneer Peeling Recovery
Many mills underestimate the direct mathematical relationship between debarker rounding quality and rotary peeling recovery:
| Metric | Sub-Standard Manual / Ring Debarker | Hanvy Dual-Roller Hydraulic Debarker |
|---|---|---|
| Log Centering Alignment | Manual / approximate (±15 mm) | Precision automatic optical/laser (±2 mm) |
| Bark Removal Cleanliness | 85% – 92% (leaves embedded dirt) | > 98.5% (clean outer wood exposed) |
| Peeling Knife Life Between Grinds | 2 – 4 hours | 8 – 12 hours (knife lasts 3x longer) |
| Time to First Usable Continuous Veneer | 35 – 55 seconds | 12 – 18 seconds |
| Timber Volume Loss During Rounding | 14% – 20% | 8% – 12% (up to 8% higher log recovery) |
| Processing Speed | 1 – 2 logs/min | Up to 3 – 5 logs/min (high speed) |
When a log is rounded into a concentric cylinder before entering the lathe, the peeling lathe knife engages immediately in full-width, continuous ribbon peeling. This eliminates minutes of producing worthless broken pieces ("fish tails") and directly increases high-value continuous face veneer yield.
3. 4 Key Engineering Factors Influencing Debarker Efficiency
Factor 1: Proportional Hydraulic Pressure Regulation
Different wood species require radically different blade pressures. Softwoods (like radiata pine or poplar) require moderate downward pressure (4–6 MPa) to prevent the knife from burying itself too deeply. Dense tropical hardwoods (like eucalyptus, keruing, or acacia) require high hydraulic clamping forces (8–12 MPa) to cleanly slice tough stringy bark and hard knots.
Factor 2: Variable Frequency Drive (VFD) Log Rotation Speed
As the log is rounded and its diameter decreases, a fixed rotation speed causes linear surface cutting speed to drop. Hanvy debarkers incorporate inverter-controlled motors that automatically accelerate roller RPM as the log slims down, maintaining constant peripheral cutting speed.
Factor 3: Integrated Driven Chain Conveyor and Log Kickers
Manual log handling creates dead time between cycles. An efficient debarker station must include:
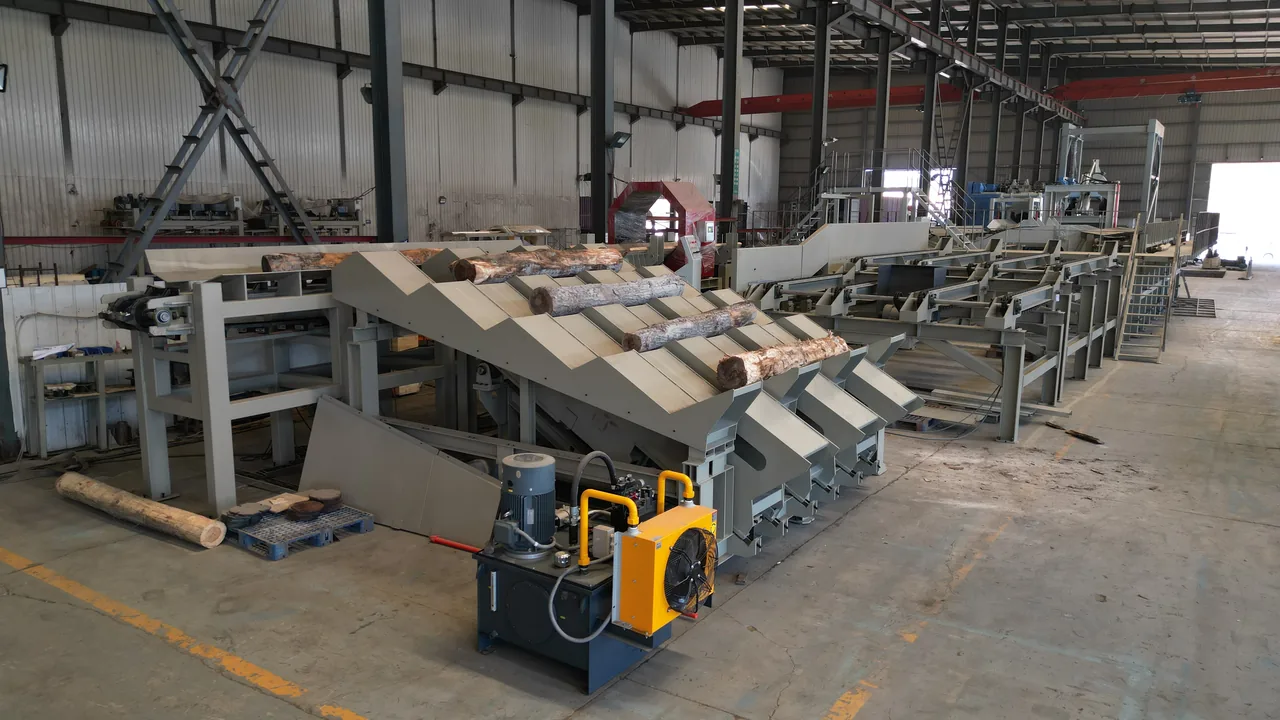
- ✓Heavy-duty powered infeed log decks to queue timber;
- ✓An automatic optical centering loader that drops the log squarely onto the roller centerline;
- ✓High-speed hydraulic kickers that eject the rounded log toward the lathe conveyor in less than 2.5 seconds.
Factor 4: Waste Bark Extraction Conveyors
A commercial 8-foot debarker removes tons of wet bark every hour. Without high-capacity underneath belt or scraper conveyors, accumulating bark wraps around drive shafts and jams roller bearings, forcing unscheduled downtime. Clean bark can be routed directly to the mill's biomass boiler to power the veneer drying line.
4. Maintenance Best Practices for Extended Machine Life
- 1Daily Knife Inspection & Honing:
Clean and deburr the debarking knife edge every shift. A dull knife tears rather than cuts, doubling hydraulic strain and power consumption.
- 1Roller Tooth De-clogging:
Inspect the knurled drive rollers weekly for embedded bark fibers or resin buildup using high-pressure steam or wire brushes.
- 1Hydraulic Oil Filtration:
Change hydraulic return filters every 1,000 operating hours to protect proportional control valves from micro-contamination.
5. Frequently Asked Questions (FAQ)
What log diameter range can a Hanvy hydraulic debarker handle?
Standard Hanvy models process logs from 100 mm up to 800 mm (or custom up to 1200 mm) in diameter, with standard log lengths of 4 feet (1300 mm), 5 feet (1600 mm), and 8 feet (2600 mm).
Can the debarker process severely curved or crooked logs?
Yes. The hydraulic floating cutterhead features an articulated self-aligning pivot that traces the longitudinal curvature of crooked logs without stalling the main drive motors.
Boost Your Mill's Timber Recovery Today
Upgrade to a Hanvy high-torque CNC hydraulic log debarker and protect your peeling lathe knives while gaining up to 8% more usable veneer from every tree trunk.
Equipo de Ingeniería de Hanvy Machinery
Diseñado con más de 30 años de experiencia en maquinaria para contrachapado. Más de 500 plantas llave en mano instaladas en 69 países.
Guías Industriales Recomendadas

Línea de Desenrollo de Chapa sin Husillo: Comparativa 4 ft vs. 8 ft, Capacidad y Rentabilidad
Análisis económico y productivo para tornos de chapa de 4 y 8 pies: ahorro de hasta $990 por turno en madera y configuración de líneas continuas.

Secador de Rodillos vs. Malla: Costos Energéticos, Producción y Guía de Selección
Especificaciones y ventajas mecánicas de secadores Hanvy: rodillos sin costura de 100 mm, cojinetes de PTFE autolubricados y rendimiento por metro cúbico.
Prensa Hidráulica Automática de Contrachapado: Optimización de Ciclos y Curvas de Presión
Control avanzado de prensado en caliente: etapas de compresión, respiración para escape de vapor y garantía de resistencia mecánica según normas EN/ASTM.