Автоматический горячий пресс для фанеры: оптимизация циклов прессования и кривых давления
Инженерное руководство по расчету и оптимизации циклов горячего прессования фанеры, ступенчатых кривых давления и фаз дегазации без брака.
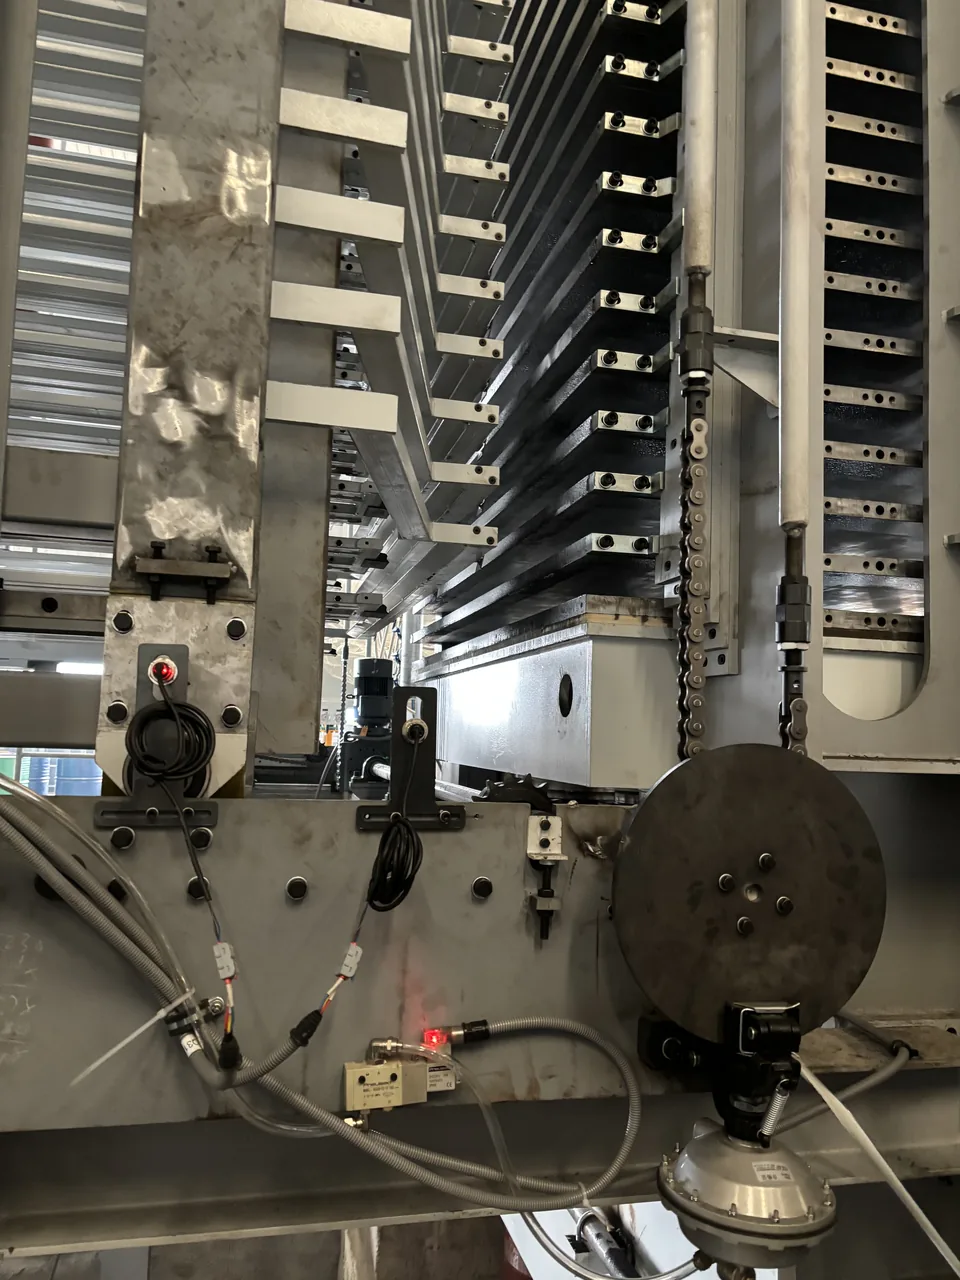
In industrial plywood manufacturing, the hot pressing stage is the defining chemical and physical transformation of the process. It is here that raw wood veneers, thermosetting resin adhesive, heat, and hydraulic force consolidate into a rigid, structural composite panel.
The hot press also represents one of the largest capital investments in a plywood plant. Any error in cycle programming produces costly panel defects:
- ✓Insufficient pressing time or temperature: Incomplete resin polymerization ("under-curing"), causing panel delamination, low MOR/MOE bending strength, and bubbling.
- ✓Excessive press time: Over-densifies outer veneers, wastes thermal energy, burns panel surfaces, and slashes whole-plant daily output.
- ✓Improper decompression rate: Trapped steam inside the panel ruptures the outer face layers upon platen opening, creating violent "blowouts" (blisters).
This engineering guide explains how to calculate, configure, and optimize the hydraulic pressure curve, temperature profile, and breathing cycle of modern multi-daylight automatic plywood hot press machines.
1. The 4 Phases of an Optimized Hot Press Cycle
A modern automated PLC hot press does not simply close and apply maximum force. Instead, it follows a pre-programmed multi-stage pressure curve:
| Pressing Phase | Operating Pressure | Typical Duration | Engineering Function |
|---|---|---|---|
| Phase 1: Fast Closing | Low (Pump idle) | 15 – 25 seconds | Rapid platen closure to prevent glue pre-cure on outer veneers |
| Phase 2: High Pressure Bonding | 1.2 – 2.0 MPa | 60% of total cycle | Densification, heat transfer to core, resin flow |
| Phase 3: Stepped Pressure Relief | 0.6 – 0.9 MPa | 25% of total cycle | Breathing stage: Controlled steam release along panel edges |
| Phase 4: Final Decompression | 0 MPa (Exhaust) | 15 – 30 seconds | Slow hydraulic bleed to eliminate blister explosions |
Stage 1: Fast Closing and Initial Contact (Low Pressure)
- ✓Goal: Close platens quickly to avoid pre-curing ("pre-cure skin") of the glue on the outer platen-facing veneers before full pressure is engaged.
- ✓Action: High-flow hydraulic auxiliary cylinders close the multi-opening rack in 15 to 25 seconds.
Stage 2: High Pressure Compression & Heat Transfer
- ✓Goal: Overcome veneer surface roughness, force close contact between all adhesive lines, and transfer platen heat deep into the panel core.
- ✓Specific Pressure: 1.0 MPa to 1.6 MPa (10 to 16 kg/cm²) for softwoods; 1.4 MPa to 2.2 MPa for dense hardwoods.
Stage 3: Stepped Pressure Reduction (Breathing / Degassing)
- ✓Goal: Release vapor pressure without blowing out the panel. As resin cures and moisture vaporizes, internal steam pressure climbs up to 0.4–0.8 MPa.
- ✓Action: The hydraulic system reduces main cylinder pressure by 30% to 50% in two programmed steps, allowing steam to escape along panel edges without rupturing the curing glue line.
Stage 4: Slow Decompression and Synchronous Opening
- ✓Goal: Final steam exhaust before platen clearance.
- ✓Action: Simultaneous platen opening mechanism ensures all daylight openings separate evenly, preventing top or bottom panels from sticking to hot steel platens.
2. Calculating Hot Press Time per Panel Thickness
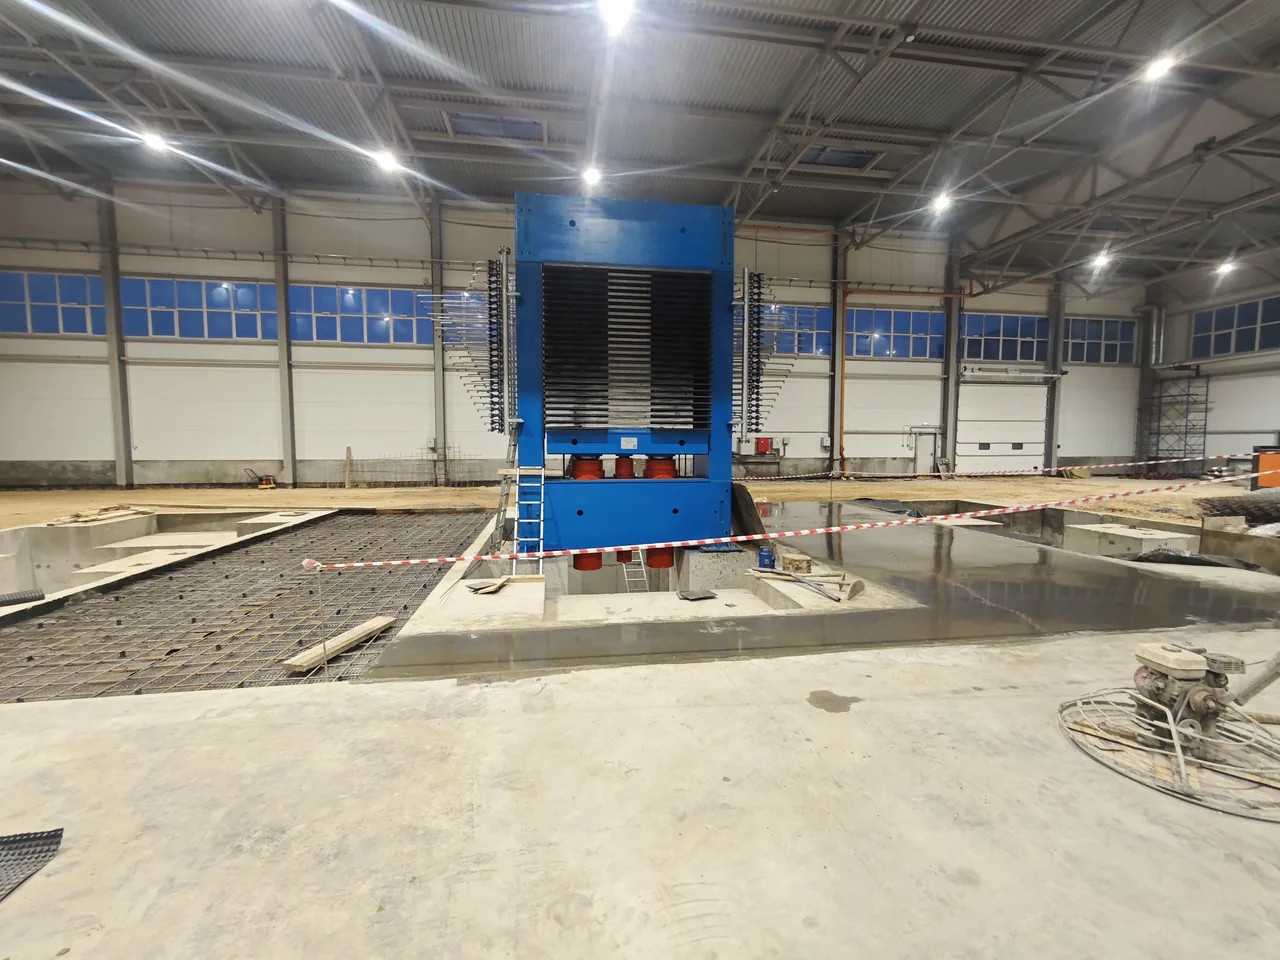
While exact timing depends on adhesive resin formulation (UF, MUF, or PF), moisture content, and wood density, industrial mill engineers calculate baseline press cycles using this standard formula:
Benchmark Curing Times by Resin Formulation
| Adhesive Resin Type | Platen Operating Temp | Heat Factor K (sec/mm) | Benchmark Press Time (18mm Panel) |
|---|---|---|---|
| Urea-Formaldehyde (UF) | 110°C – 125°C | 45 – 60 seconds/mm | 14 – 18 minutes |
| Melamine-Urea-Formaldehyde (MUF) | 120°C – 135°C | 50 – 65 seconds/mm | 15 – 19 minutes |
| Phenol-Formaldehyde (PF Marine Grade) | 135°C – 150°C | 55 – 75 seconds/mm | 17 – 22 minutes |
- ✓Impact of Pre-Pressed Billets:
Running assembled veneers through an automatic plywood cold press consolidates loose veneers into tight billets, allowing you to reduce subsequent hot press time by 15% to 25% and preventing face veneers from shifting during loading.
3. Upstream Quality Control: Glue Spreader and Moisture Balance
No amount of hot press tuning can fix poorly prepared veneer billets:
- 1Accurate Resin Spread Rate:
Using an automatic 4-roller glue spreader with motorized doctor rolls guarantees uniform resin distribution (typically 280–360 g/m² double-line spread). Excess glue introduces excess water, triggering steam blows.
- 1Strict Dry Veneer Moisture Content:
Before lay-up, dry veneer from your continuous jet dryer must be verified between 8% and 12%. Veneer above 14% moisture is the #1 culprit behind delamination blisters.
4. Key Mechanical Features of Hanvy Automatic Hot Presses
When selecting an industrial multi-daylight press line, verify the following specifications:
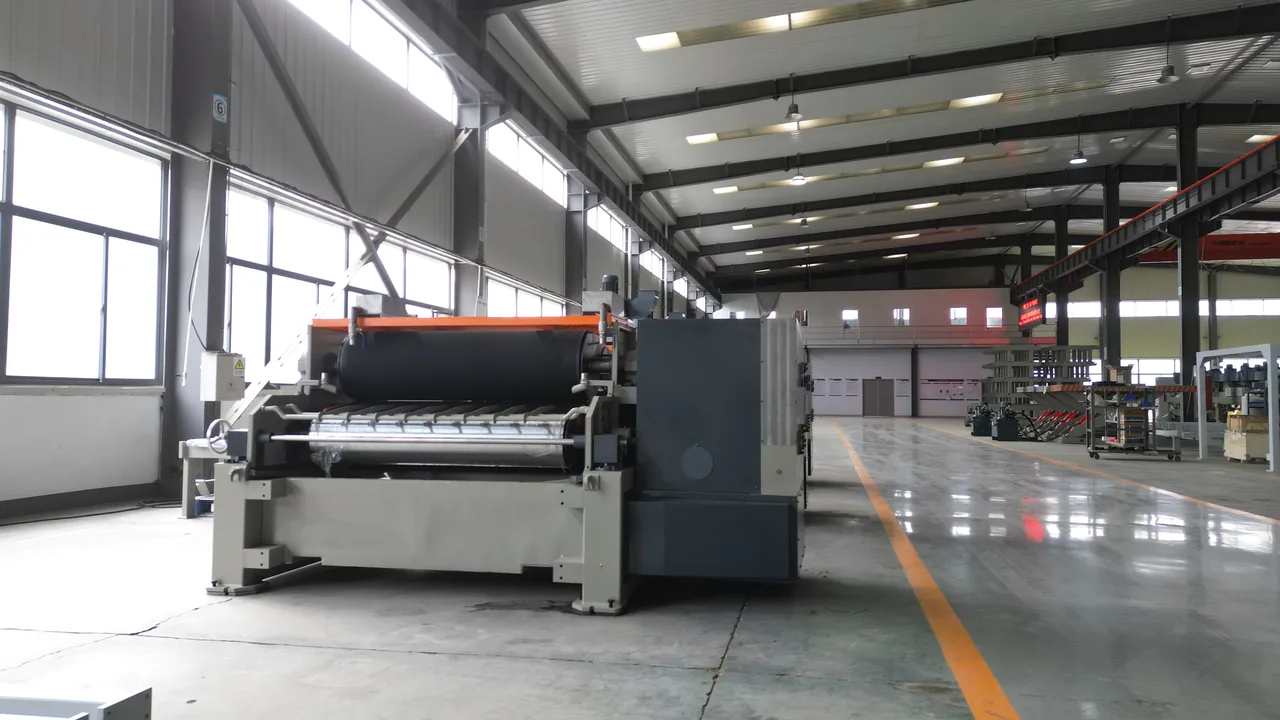
- ✓Solid Steel Drilled Platens (Q235 / Q345):
Precision double-side ground platens with deep gun-drilled serpentine heating channels guarantee temperature uniformity within ±1.5°C across the entire 4x8 ft or 5x10 ft platen surface.
- ✓Automatic Simultaneous Platen Closing Device:
Mechanical synchronous arms guarantee that all openings close and open at the identical split-second, ensuring equal heat and pressure exposure across every single board in the daylight stack.
- ✓Automatic Infeed Charger & Outfeed Discharger:
Reduces open-press dead time between batches from 4 minutes (manual) to under 45 seconds, boosting daily plant output by up to 35%.
5. Frequently Asked Questions (FAQ)
What causes plywood panels to pop or blister when the press opens?
Blisters ("steam explosions") occur when high internal steam pressure exceeds the green strength of the adhesive at the moment of platen opening. The primary causes are: (1) veneer moisture content exceeding 13%, (2) excess glue spread, or (3) decompressing the hydraulic rams too abruptly without a stepped breathing stage.
Thermal oil vs. steam: which provides better temperature control in hot presses?
Thermal oil operates at atmospheric pressure up to 250°C without risk of water hammer or pipe scaling, maintaining steady temperatures across all platens. For a comprehensive comparison, read our detailed report on Thermal Oil vs. Steam Heating for Hot Presses.
Design Your High-Capacity Hot Press Line
Hanvy Machinery manufactures 10-opening, 15-opening, 20-opening, and 25-opening heavy-duty automatic hot press lines with pressure capacities from 500 tons to 1,200 tons.
Инженерно-техническая команда Hanvy Machinery
Свыше 30 лет опыта проектирования и производства тяжелого деревообрабатывающего оборудования. Более 500 комплектных заводов в 69 странах.
Рекомендуемые отраслевые статьи

Линия лущения шпона: сравнение форматов 4 фута и 8 футов, производительность и экономика
Экономический и технический анализ линий лущения 4x4 и 4x8 футов: окупаемость вложений, экономия сырья и спецификация оборудования для фанерных комбинатов.

Роликовая или сетчатая сушилка шпона: энергозатраты, производительность и руководство по выбору
Практический выбор сушилки шпона: технические характеристики серий HG132, HG133, HG134, расход пара на кубометр и конструктивные преимущества роликов 100 мм.
Выбор бесшпиндельного лущильного станка: лущение внутреннего слоя против лицевого шпона
Настройка лущильного станка под разные типы шпона: геометрия прижимной линейки, угол заточки ножа, сервоприводы и гладкость поверхности среза.